High-Integrity Valve Assemblies: Primary Selection
Explore ZFA Valve's OEM and bespoke manufacturing capabilities engineered to eliminate water hammer, prevent dynamic backflow, and ensure zero-leakage pipeline integrity.
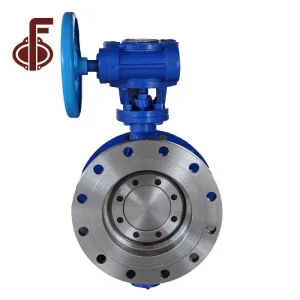
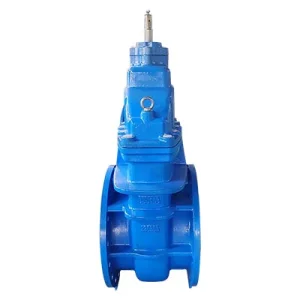
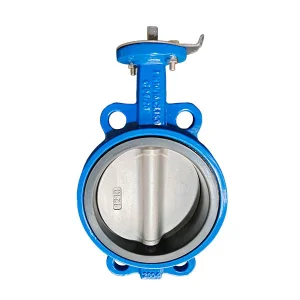
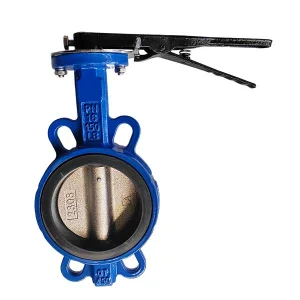
The Evolution of Swing Check Valve Engineering in China
Analyzing modern metallurgic transitions, dynamic response mechanics, and cavitation mitigation across severe industrial flow networks.
Hydrodynamic Optimization
Traditional swing check valves face premature failure due to chattering and severe water hammer induced by rapid flow deceleration. Leading Chinese manufacturers now utilize Computational Fluid Dynamics (CFD) modeling to formulate contoured disc geometries and counterweight-lever dashpot dampening assemblies.
- Minimized cracking pressure (<0.02 bar threshold)
- Optimized hinge pin positioning for accelerated closure speed
- Oblique seat angled configurations (up to 20°) shortening closure strokes
Metallurgical Advancements
Demanding chemical processing, seawater reverse osmosis (SWRO), and offshore oil and gas necessitate extreme corrosion and erosion resistance. Valve casting foundries in Tianjin are transitioning from plain carbon steels to specialized alloy metallurgies.
- Dual-certified CF8M, Duplex 2205, and Super Duplex 2507 castings
- Hardfaced Stellite 6 and nickel-base overlay sealing faces
- Electroless Nickel Plating (ENP) on hinge pins to mitigate galling
Total Life Cycle Reliability
Global procurement teams prioritize lowest Total Cost of Ownership (TCO) over basic CAPEX. By adopting precision CNC machined renewable seat rings and encapsulated hinge designs that eliminate external fugitive emissions through the bonnet joint, operational lifespans expand significantly.
- Zero fugitive emission bonnets compliant with ISO 15848-1
- Field-replaceable seats preventing pipeline despooling
- Dynamic cycle test verification exceeding 50,000 actuations
Global Enterprise Sourcing Architecture & Selection Criteria
How Tier-1 engineering procurement contractors (EPCs) and plant managers de-risk supply chains when sourcing from Chinese check valve manufacturers.
| Application Environment | Primary Engineering Failure Risk | Critical Design Requirements | Recommended Material & Trim Spec |
|---|---|---|---|
| High-Lift Municipal Pump Discharge | Reverse flow water hammer damaging rotating impellers; hinge pin fatigue. | Non-slam internal dampener, counter-weight arm with hydraulic dashpot, resilient soft seat (EPDM/NBR). | Body: EN-GJS-400-15 / WCB Disc: CF8M Seat: Replaceable EPDM / BUNA-N |
| Offshore Crude Oil Transfer | Hydrogen sulfide (H2S) stress corrosion cracking; hydrocarbon micro-leaks. | API 6D compliance, NACE MR0175/ISO 15156 adherence, full-bore piggable construction. | Body: ASTM A216 WCC / LCC Trim: 13Cr / Stellite Hardfaced Bolting: B7M/2HM |
| Chemical Processing Lines | Severe intergranular attack, acid corrosion, seat erosion under high turbulence. | Precision investment cast bodies, zero body penetrations for pin assembly, PTFE or metal-to-metal seal. | Body: ASTM A351 CF8M / CF3M Trim: Monel / Hastelloy C-276 Seat: Virgin PTFE |
| Steam & Power Generation Condensate | Thermal expansion jamming, steam wire drawing across sealing faces. | Pressure seal bonnet construction, tilted seat design, integral high-temperature hardfacing. | Body: ASTM A217 WC6 / WC9 Trim: Trim 5 (Stellite to Stellite) Rating: ASME Class 600 - 2500 |
Macro Fluid Protection Solutions Engineered by Chinese Factories
Comprehensive engineering strategies applied across mission-critical utility, energy, and process infrastructures worldwide.
Potable Water & Desalination
Protecting massive desalted water transmission pipelines from transient surge surges. Featuring full-diameter, unrestricted flow paths that deliver minimum hydraulic resistance, reducing plant pumping electricity demand by up to 8% annually.
Combined Cycle Power Plants
Boiler feed pump protection demanding absolute sealing reliability under cyclical operational modes. We configure tilting-disc non-slam check valves capable of instantaneous reseating prior to velocity reversal, averting catastrophic pressure spikes.
Refining & Heavy Petrochemicals
Supplying robust cast carbon steel and chrome-moly swing checks engineered with full-traceability foundry melts. Designed to operate safely under high partial pressure hydrogen and lethal sour gas applications.
Localized Support, Audit Readiness & Technological Roadmap
Bridging global specification standards with Chinese high-output manufacturing excellence.
Digital Casting Simulation
Integration of MAGMASOFT finite-element solidification analysis to eliminate shrinkage porosity in heavy-wall Class 900+ swing check valve castings.
Automated Cladding Cells
Robotic PTA (Plasma Transferred Arc) Stellite welding for valve seat rings and disc seating surfaces, providing micron-level deposition uniformity and crack-free overlays.
Smart Sensor Telemetry
Embedding acoustic emission and disc position transmitters directly into counterweight dashpot brackets for real-time SCADA predictive maintenance reporting.
Zero Emission Certification
Standardizing all flanged and pressure-seal bonnet swing check valve designs to ISO 15848-1 Class AH emission thresholds for green hydrogen deployment.
Frequently Asked Questions: Swing Check Valves
Direct technical answers from factory valve design specialists.
Q: What causes water hammer in swing check valves and how is it prevented?
A: Water hammer occurs when the valve disc does not reach its seat prior to reverse flow acceleration. Once flow reverses, the disc slams shut into the fluid column, generating high-velocity pressure waves. Chinese OEM factories mitigate this via tilted disc seating, counterweighted lever arms, or external hydraulic snubbers that decelerate final disc travel.
Q: Can swing check valves be installed in vertical piping lines?
A: Yes, but strictly in vertical lines with upward fluid flow. In upward flow, gravity assists the closing motion when flow stops. Swing check valves must never be installed in vertical lines with downward flow, as gravity will hold the disc open or cause unstable flutter.
Q: How do Chinese manufacturers verify casting integrity?
A: Quality-oriented factories execute 100% PMI (Positive Material Identification) on pressure-retaining components, complemented by Non-Destructive Testing (NDT) such as Radiographic Testing (RT) per ASME B16.34 Appendix I, Ultrasonic Testing (UT), and Magnetic Particle Inspection (MPI) on critical flanged junctions.
Q: What is the advantage of an internal hinge pin design?
A: An internal hinge pin is mounted entirely inside the valve body cavity, eliminating through-wall body holes and companion hinge pin plugs. This zero-penetration architecture removes potential external leak paths, maximizing safety in toxic, volatile hydrocarbon, and corrosive applications.
High-Integrity Valve Assemblies: Advanced Catalog
Complete project-ready industrial flow control configurations produced in accordance with ASTM, ANSI, ISO, BS, DIN, GOST, JIS, and KS manufacturing codes.