
Industrial Gate & Quarter-Turn Valve Solutions
Engineered for direct automation integration across water distribution, hydrocarbon processing, marine service, and thermal power lines.
The Engineering Paradigm of OEM Actuated Gate Valves
Balancing zero fugitive leakage, thrust safety margins, and autonomous digital fieldbus protocols in modern piping automation.
In modern automated processing lines, the manual isolation gate valve has evolved into an instrumented, electro-mechanically driven control asset. An actuated gate valve pairs a linear rising or non-rising stem valve body—commonly resilient seated wedge gate or solid parallel slide configuration—with an intelligent multi-turn actuator (electric, pneumatic cylinder, or electro-hydraulic). Unlike quarter-turn ball or butterfly valves, an actuated gate valve provides an unobstructed full-bore conduit when fully retracted, resulting in virtually negligible pressure drops ($\Delta P \approx 0$) and zero cavity cavitation during full laminar transfer.
For international procurement officers, engineering, procurement, and construction (EPC) contractors, and private-label valve brands, selecting a qualified OEM actuated gate valve manufacturer requires strict technical scrutiny beyond mere pricing. Actuated service introduces severe cyclic dynamic torsional and axial thrust loads upon the valve stem, yoke, bonnet bolts, and wedge guides. As an established manufacturer operating from Tianjin, China since 2006, Tianjin Zhongfa Valve Co., Ltd. (ZFA Valve) operates fully audited foundry casting, CNC turning, ISO 5210 top flange machining, actuator mounting, and pressure testing under strict ISO 9001 and CE (PED 2014/68/EU) certified quality regimes.
Engineering Insight: Thrust Calculation and Sizing Coefficients
An actuated gate valve must overcome running friction, packing box compression, differential pressure force ($F_{dp} = \Delta P \times A_{seat}$), and disc-to-seat friction ($\mu \approx 0.3$ for metal-to-metal, $0.15$ for elastomeric resilient seats). A qualified OEM factory calculates the exact operating thrust and applies a minimum safety factor of 1.3 to 1.5 across high ambient variations to prevent actuator motor stall or stem deformation.
Mission-Critical Localized Application Scenarios
Tailored trim metallurgy, enclosure ratings, and stroke cycling designed for specific regional working conditions.
Municipal Water & Desalination
Large-diameter ductile iron (QT450/GGG50) resilient seated gate valves fitted with IP68 submersible electric multi-turn actuators. Fully encapsulated EPDM wedges provide bubble-tight Class A bi-directional sealing. In coastal seawater reverse osmosis (SWRO) intake arrays, custom nickel aluminum bronze (C95800) or Super Duplex stainless steel bodies prevent pitting and galvanic corrosion.
Thermal Power & District Energy
High-pressure forged steel (A105, F22) or cast carbon steel (WCB, WC6/WC9) flexible wedge gate valves built for superheated steam mains and boiler feed water isolation. Paired with fast-closing fail-safe electro-hydraulic actuators featuring high-temperature ceramic stem extensions and Stellite No. 6 hardfaced seats to eliminate wire-drawing erosion under extreme thermal expansion.
Petrochemical & Refining Terminals
API 600 bolted bonnet rising stem gate valves with flexible wedges and low-emission graphite stem packing compliant with ISO 15848-1. Actuators are ATEX and IECEx certified explosion-proof (Ex d IIB/IIC T4) units with remote DCS Modbus or Profibus fieldbus feedback, engineered to isolate high-viscosity hydro-cracker bottoms, tank farms, and vapor recovery headers.
Future Trends in Gate Valve Actuation & Smart Diagnostics
Where mechanical engineering converges with edge computing, non-intrusive commissioning, and smart predictive maintenance.
IoT Edge Diagnostics
Integration of Hall-effect torque sensors and acoustic emission transducers directly within the actuator housing to record real-time thrust curves, detecting seating galling or scale accumulation before plant outages.
SIL3 Functional Safety
Dual-redundant microcontrollers, self-testing solenoid blocks, and Partial Stroke Testing (PST) logic enabling critical Emergency Shutdown (ESD) gate valves to test wedge movement by 10% without disrupting line pressure.
Ultra-Low Fugitive Emissions
Adoption of live-loaded chevron PTFE and expanded graphite packing systems achieving ISO 15848-1 Class AH ratings (≤10−6 mg/(s·m)), preventing volatile organic compound (VOC) leakage across 10,000 mechanical strokes.
Digital Twin Modeling
OEM parametric FEA stress modeling synchronized with actuator output data, enabling automated life-cycle prediction for high-pressure gate valves operating in cyclic thermal environments up to 550°C.
China OEM Supply Chain Resilience & Production Depth
How Tianjin Zhongfa Valve integrates foundry control, modular machining, and rapid automated assembly.
Global supply chain disruptions have highlighted the strategic vulnerability of long-lead valve sourcing. As an established OEM manufacturing base in Tianjin—China's historical coastal valve engineering hub—ZFA Valve leverages an integrated, multi-tier industrial cluster. From sand mold casting and lost-wax investment casting foundries to multi-axis CNC horizontal boring mills, raw castings are transformed into calibrated actuated valve assemblies under unified quality supervision.
Foundry & Metallurgy Autonomy
Direct ownership of spectroscopic metallurgical verification (OES) guarantees chemistry compliance for ductile iron (QT450-10), WCB, CF8, CF8M, and Bronze before pouring, eliminating hidden porosities and casting inclusions.
Actuation Interoperability
Standardized ISO 5210 multi-turn and ISO 5211 quarter-turn mounting flange design allows ZFA bodies to mate seamlessly with premier international actuation brands (AUMA, Rotork, Bernard, Limitorque) as well as cost-effective proprietary OEM intelligent drives.
Agile Lead-Time Scaling
Standardized raw cast inventory allows valve body machining and assembly within 15–25 business days for standard pressure ratings (PN10/16, Class 150/300), minimizing EPC construction milestone delays across global ports.
OEM Actuated Gate Valve Technical Matrix
Cross-standard engineering parameters for project datasheets and OEM brand private labeling.
| Parameter / Dimension | Resilient Seated Wedge Gate | Flexible Wedge Cast Steel Gate | Parallel Slide Knife / Slurry Gate |
|---|---|---|---|
| Nominal Diameter | DN50 – DN1200 (2" – 48") | DN50 – DN900 (2" – 36") | DN50 – DN1500 (2" – 60") |
| Pressure Rating | PN10, PN16, PN25, Class 125/150 | Class 150, 300, 600, 900 (PN20 – PN150) | PN6, PN10, PN16, Class 150 |
| Design Standards | EN 1074-1/2, DIN 3352, AWWA C509/C515 | API 600, ASME B16.34, ISO 10434 | MSS SP-81, TAPPI-TIS 405 |
| Body Metallurgy | Ductile Iron (GGG50 / QT450-10) | WCB, LCC, WC6, WC9, CF8, CF8M | WCB, CF8, CF8M, Duplex 2205 |
| Actuation Mount Interface | ISO 5210 Multi-turn (F10 to F30) | ISO 5210 / Customized Yoke Flange | ISO 5211 / Direct-Mount Linear Bracket |
| Sealing Classification | EN 12266-1 Rate A (Zero Leakage) | API 598 Metal-to-Metal / Rate A Soft Seat | MSS SP-81 or Class V / Rate A Resilient |
| Applicable Media | Potable water, sewage, chilled HVAC, neutral slurries | Crude oil, high-pressure steam, refined fuels, gas | Mining tailings, paper pulp, ash handling, powder bulk |
Global Commercial Landscape & Localized Compliance
Navigating regional testing standards, documentation packs, and on-site factory acceptance testing (FAT).
North America (ASME / API / AWWA)
Compliance with ASME B16.34 wall thickness and API 600 stem diameter minimums is critical. Actuators require Class I, Div 1/2 hazardous location explosion-proof approvals (UL/FM) and AWWA C541 actuation conformity for municipal utility tenders.
Europe & UK (CE / PED / WRAS)
Valves supplied into the EEA demand CE marking under Pressure Equipment Directive (PED 2014/68/EU) Module H conformity. Drinking water installations require hygienic certification for non-metallic elastomer linings (WRAS, ACS, DVGW W270).
Middle East & Harsh Environments
Projects across Aramco, ADNOC, and GCC utilities stipulate NACE MR0175/ISO 15156 sour gas trim hardness limits (≤22 HRC) along with high-ambient solar radiation enclosures, sand-storm filtration IP68 protection, and 100% radiography (RT) on pressure boundaries.
Frequently Asked Questions · OEM Procurement
Engineered responses addressing technical inquiries from purchasing managers, pipeline consultants, and valve distributors.
What parameters are essential when ordering an OEM actuated gate valve package?
To accurately size both the gate valve body and actuator, the OEM manufacturer requires: nominal line size (DN/NPS), pipeline design and operating pressure ($\Delta P$ across the gate), operating medium (liquid, dry steam, abrasive slurry), media operating temperature range, flange drilling standard (ANSI Class 150/300, DIN PN10/16, JIS 10K), power supply parameters (400V 3-phase, 220V 1-phase, 24V DC, or instrument air pressure for pneumatic sets), and control signals (on/off 4-20mA analog modulating, or digital fieldbus protocols such as Modbus, Profibus DP, Foundation Fieldbus).
How does ZFA Valve guarantee dimensional accuracy and stem-to-actuator concentricity?
Misalignment between the rising valve stem and the actuator drive sleeve creates side-thrust wear, premature gland packing destruction, and accelerated motor burnout. At our Tianjin factory, we execute the machining of the valve bonnet mounting face, stem hole, and ISO 5210 actuator mounting flange in a single clamping setup using high-precision CNC horizontal machining centers. Concentricity is held within ±0.02 mm, ensuring purely axial stem thrust during stroke travel.
Can ZFA Valve customize valve nameplates, coatings, and private branding for OEM customers?
Yes. True OEM contract manufacturing comprises custom stainless steel 316 nameplates etched with your brand identity, part numbering system, and QR-coded serial numbers linked directly to Mill Test Reports (MTR EN 10204 3.1). Furthermore, we offer custom RAL epoxy painting options—including high-build polyurethane coatings and heavy-duty C5M marine grade coatings compliant with ISO 12944—tailored to specific engineering project specifications.
What is the key difference between rising stem (OS&Y) and non-rising stem (NRS) actuated gate valves?
In an Outside Screw and Yoke (OS&Y) rising stem valve, the stem threads reside outside the wetted fluid path. As the actuator turns the drive nut, the stem moves linearly upward. This provides clear visual position indication and shields critical threads from corrosive fluids; however, it requires greater vertical clearance. Non-rising stem (NRS) valves maintain a constant height, making them ideal for underground chambers, marine engine rooms, or confined skids, but are restricted to relatively non-scaling media.
What Factory Acceptance Testing (FAT) documentation accompanies each valve shipment?
Every production lot undergoes 100% hydrostatic shell testing (1.5 × PN) and bi-directional seat leakage testing (1.1 × PN) according to ISO 5208 and API 598 before shipment. Each shipment is accompanied by a full technical documentation dossier containing EN 10204 3.1 material chemical & mechanical test certificates, coating thickness dry-film inspection reports, actuator calibration and torque curve certificates, and CE conformity declarations.
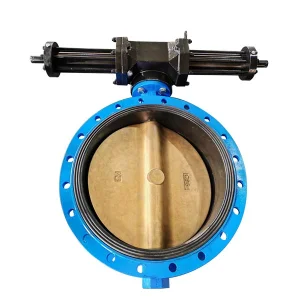
Comprehensive Automated & Auxiliary Valves
Engineered for direct project specification, wholesale distribution, and turn-key EPC skid fabrication.
Configure Your Actuated Gate Valve Package Today
Connect directly with our valve design engineers in Tianjin. Submit your pipeline datasheets, medium specifications, and actuator interface requirements for an authoritative engineering review and formal quotation within 24 hours.
