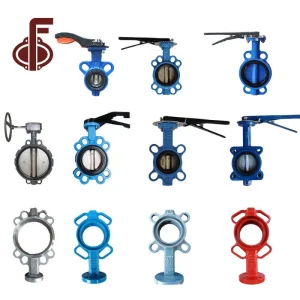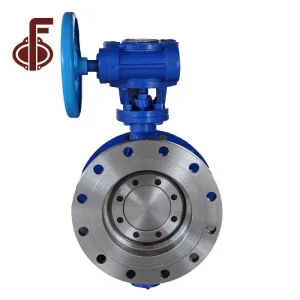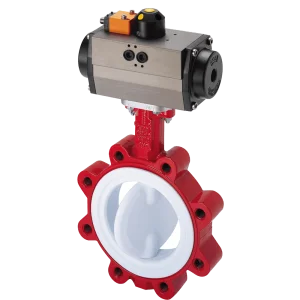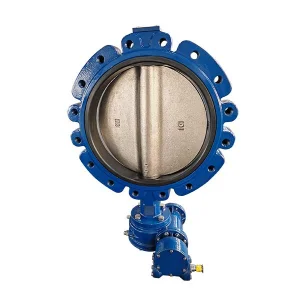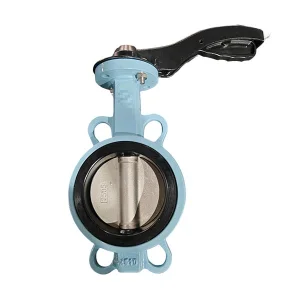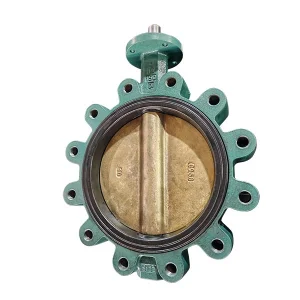
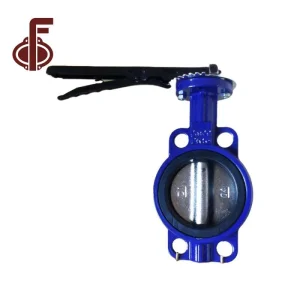
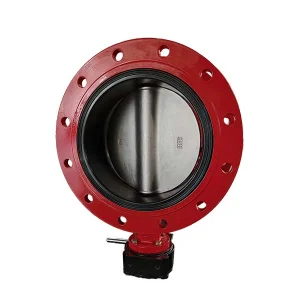
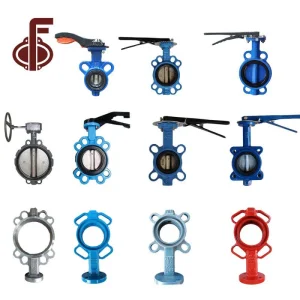
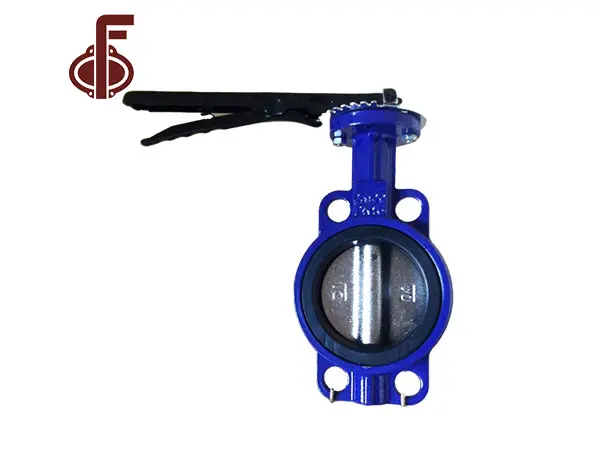
Ductile Iron Wafer Butterfly Valve with Aluminum Handle Production
A step-by-step review of precision machining, electrostatic epoxy powder coating, manual lever assembly, and high-efficiency production balancing.
Read Full GuideDirect factory configurations engineered for bidirectional bubble-tight sealing, low hydrodynamic torque, and long operating lifecycle in extreme municipal and industrial installations.
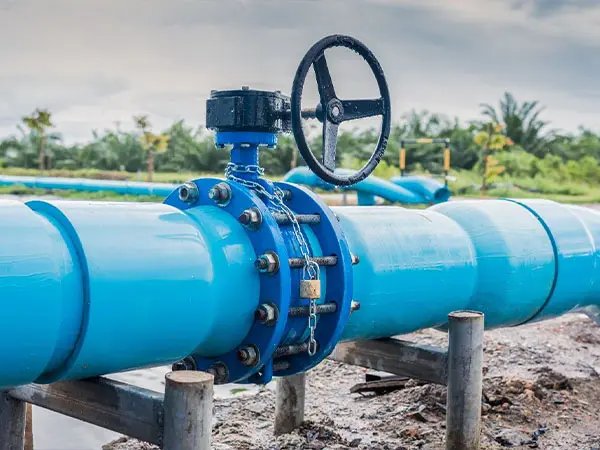
An in-depth metallurgical assessment of why Ductile Iron (EN-GJS-400-15 / ASTM A536 65-45-12) serves as the definitive structural standard for high-cycle industrial quarter-turn valves.
Unlike brittle gray cast iron (GG25) with flake graphite that concentrates internal stress, Ductile Iron (DI) utilizes magnesium nodulizing inoculants during ladle treatment. This creates spherical graphite nodules that arrest crack propagation, increasing tensile strength above 400 MPa and providing elongation up to 15-18%.
Transient pressure spikes and mechanical vibrations from rapid valve closure can shatter standard cast alloys. Ductile iron bodies possess superior Charpy impact resilience and fatigue resistance, providing safety margins up to PN25 rated working pressures across potable water, sewage, and fire fighting loops.
DI castings undergo automated shot blasting to ISO 8501-1 Sa 2.5 profile prior to electrostatic fluidized-bed Fusion Bonded Epoxy (FBE) powder coating (min 250 μm). The chemically bonded inert barrier prevents cathodic oxidation, galvanic de-alloying, and aggressive bio-fouling in buried or submerged installations.
| Material Property | Ductile Iron (QT450-10 / GGG40) | Ductile Iron (QT500-7 / GGG50) | Gray Cast Iron (HT200 / GG25) | Cast Carbon Steel (WCB / 1.0619) |
|---|---|---|---|---|
| Tensile Strength (MPa) | ≥ 400 MPa Optimal Toughness | ≥ 500 MPa High Load | ≥ 200 MPa (Brittle Fracture Risk) | ≥ 485 MPa |
| Yield Strength (MPa) | ≥ 250 MPa | ≥ 320 MPa | No measurable yield point | ≥ 250 MPa |
| Elongation at Break (%) | ≥ 15% (Superior Ductility) | ≥ 7% | < 0.8% (Negligible Plasticity) | ≥ 22% |
| Charpy V-Notch Impact (J) | ≥ 12 J at -20 °C | ≥ 10 J at Room Temp | Near Zero Impact Energy | ≥ 27 J at -29 °C |
| Cost vs. Performance Ratio | Industry Benchmark | Economical High Pressure | Low Cost / High Field Failure | High Cost / Heavy Weight |
In ductile iron butterfly valves, the elastomer or polymer liner acts as both the boundary fluid seal and the internal body protector. Specifying the incorrect compound causes swelling, embrittlement, or destructive torque excursions.
| Seat Compound | Working Temp (°C) | Shore A Hardness | Optimum Line Media | Contraindicated Chemical Fluids | Compliance Marks |
|---|---|---|---|---|---|
| EPDM (Peroxide Cured) | -20 °C to +135 °C | 70 ± 5 | Potable drinking water, treated wastewater, chilled/hot glycol HVAC loops, aeration lines. | Hydrocarbons, mineral oils, petroleum distillates, diesel fuel, halogenated solvents. | WRAS / NSF-61 / DVGW |
| NBR (Buna-N / Nitrile) | -15 °C to +90 °C | 75 ± 5 | Crude oily water, petroleum lubricating fluids, air with compressed oil mists, diesel lines. | Polar solvents, acetone, strong oxidizing acids, brake fluids, UV/ozone exposure. | EN 682 Class G |
| PTFE (Virgin / Filled) | -25 °C to +180 °C | 55 ± 5 Shore D | Aggressive acids (sulfuric, hydrochloric), alkaline caustic lyes, ultra-pure pharma solutions. | Molten alkali metals, high fluorine gas under pressure, heavily abrasive slurry. | FDA CFR 21 / USP VI |
| FKM (Viton® Fluoroelastomer) | -10 °C to +200 °C | 75 ± 5 | High-temperature synthetic lubricants, harsh chemical fuels, aromatic hydrocarbons. | Low molecular organic acids (formic, acetic), ammonia, polar ethers. | High Thermal Grade |
The elastomer is directly injected and vulcanized to the ductile iron body casting under extreme heat and pressure. Eliminates liner slipping and bunching during high-velocity throttling; recommended for vacuum conditions down to 0.01 bar absolute.
Constructed with an elastomer compound molded around a rigid phenolic or aluminum backing ring. Prevents radial collapse, enables field replacement in remote project locations without replacing the valve casting, and stabilizes torque ratings.
Precision isostatic compression molded PTFE minimum 3.0mm thickness supported by a resilient silicone or EPDM energizer pad. Completely isolates the ductile iron casing from aggressive acids, high-purity water, and corrosive chemical washouts.
Operating from Tianjin—the premier valve manufacturing cluster of Northern China—Tianjin Zhongfa Valve Co., Ltd. integrates automated resin sand molding lines, 5-axis CNC machining centers, and 100% digital traceability.
Automated flaskless molding produces DI castings with dimensional tolerances adhering to ISO 8062-3 CT7, minimizing porosity, core shift, and surface inclusion defects.
Dedicated horizontal boring and CNC machining centers turn body bores, flange gasket grooves, and stem journal tolerances to ±0.015mm, guaranteeing coaxial disc centering.
Every DI valve undergoes double-side hydro shell testing at 1.5× PN rating and bidirectional pneumatic seat testing at 1.1× PN under ISO 5208 Rate A (zero detectable bubbles).
Laser engraving, custom SS304 nameplates with client valve tags, casting logo tooling, custom RAL powder coating, and export plywood crating meeting ISPM-15 phytosanitary rules.
From seawater reverse osmosis plants in the Middle East to district energy networks across Northern Europe, ZFA valves deliver application-tailored hydrodynamic reliability.
High chloride environments induce pitting and crevice corrosion in standard valves. We engineer DI bodies paired with nickel-aluminum bronze (C95800 / ASTM B148) or 2507 super duplex discs and high-grade peroxide-cured EPDM seats, resisting aggressive brine and marine cavitation.
Modern building services demand tight balance control and zero thermal dissipation. Our concentric and double eccentric DI butterfly valves with ISO 5211 top flanges pair seamlessly with electric modulating actuators, providing linear flow characteristics and 50,000+ zero-leakage cycles.
Underground pipelines cannot accommodate frequent valve servicing. ZFA manufactures large-diameter double-flanged ductile iron butterfly valves up to DN2400 with internal and external WRAS-approved epoxy coatings, stainless steel 316 shafts, and self-lubricating PTFE bushings.
Flow control infrastructure is rapidly digitizing. ZFA's engineering research team is driving innovations across smart diagnostic actuation, fugitive emissions reduction, and advanced composite fluid dynamics.
Integration of wireless smart stem-torque sensors and acoustic cavitation monitors into DI butterfly valve top-works. Real-time feedback transmits torque decay, cycle counters, and disc position over Modbus or LoRaWAN, enabling predictive maintenance prior to seal fatigue.
Meeting stringent ISO 15848-1 and TA-Luft Class AH standards via redundant dynamic stem sealing: primary quad-ring elastomer boundary backed by live-loaded PTFE chevron V-rings and secondary O-ring dust seals, guaranteeing leakage rates <10⁻⁴ mbar·l/(s·m).
Utilizing high-performance computational fluid dynamics (CFD) to redesign disc thickness profiles and leading edges. Reduces valve pressure drop (ΔP), elevates flow coefficient (Cv/Kv) by 18-24%, and minimizes flow-induced turbulence and noise across pump discharge lines.
Experienced EPC contractors evaluate valves beyond the initial purchase order price. Field failure, replacement labor, pipeline shutdown hours, and actuator torque degradation dominate actual life-cycle expenditure.
| Evaluation Parameter | Tier 1: ZFA Valve OEM Standards | Low-Cost Non-Compliant Workshops | Operational Impact & Risk Mitigation |
|---|---|---|---|
| Casting Body Material | Ductile Iron QT450-10 with chemical spectrographic analysis & heat code. | Recycled scrap cast iron or un-inoculated grey iron marked as "DI". | Eliminates sudden body cracking during thermal expansion or water hammer. |
| Stem Retention / Connection | Double-D, spline, or square pinless drive with anti-blowout stem design. | Crude taper pins driven through disc & stem creating leak paths. | Guarantees zero fluid migration through disc pins and prevents stem ejection. |
| Liner Material Purity | 100% virgin raw elastomer compound (EPDM polymer content ≥ 45%). | Elastomers heavily cut with carbon black filler and recycled rubber crumb. | Maintains elastic memory, preventing seat compression set and high torque spikes. |
| Coating Standards | Automated electrostatic FBE coating ≥ 250 μm, holiday spark tested at 3kV. | Manual air-sprayed alkyd primer (< 60 μm) prone to pinholes. | Guarantees 25+ years corrosion barrier in aggressive soils and damp vaults. |
| Testing Protocols | 100% hydro shell (1.5x) & seat (1.1x) with automated data-logging. | Spot testing 1 in 20 units or unverified test certificates. | Eliminates costly site de-installation, pipeline re-welding, and warranty claims. |
Valve products must drop seamlessly into engineering design schedules across North America, Europe, the Middle East, and Asia without redesigning flange bolt circles or face-to-face dimensions.
Universal bolt hole patterns compatible with EN 1092-2 PN10/PN16, ASME B16.1 Class 125/150, and JIS B2239 10K, simplifying global inventory skids.
Strict conformance to ISO 5752 Basic Series 20, EN 558 Series 20, and API 609 Table 1 for wafer, lug, and double-flanged bodies.
Standardized ISO 5211 actuator mounting pads with double-D or keyed shaft profiles, allowing direct-mount manual levers, worm gearboxes, pneumatic, or electric actuators.
Audited quality systems under ISO 9001:2015, Pressure Equipment Directive (PED 2014/68/EU) CE mark, and complete EN 10204 3.1 material test certs.
In-depth technical guides authored by our chief foundry metallurgists and applications engineers to assist EPC specifiers and plant operations staff.
A step-by-step review of precision machining, electrostatic epoxy powder coating, manual lever assembly, and high-efficiency production balancing.
Read Full Guide
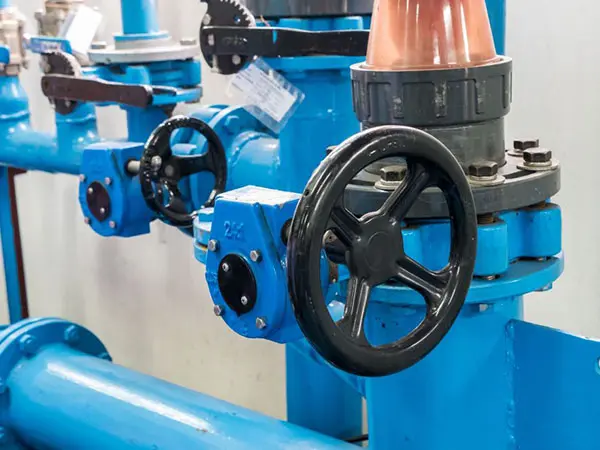
Comparing wafer clamping, independent threaded lug bolting, and double-flanged installations under dynamic line strain and thermal movement.
Read Full Guide
Evaluating stress distribution, corrosive galvanic leakage around taper pins, and why pinless polygon or splined drive shafts offer superior reliability.
Read Full GuideDetailed technical responses addressing engineering specifications, materials science, installation practices, and OEM procurement queries.
Specialty metallurgical selections, high-pressure ratings, and actuated flow isolation solutions engineered for severe chemical, power, and high-volume industrial pipelines.
Submit your valve schedules, pipeline engineering drawings, or OEM customization requirements directly to our Tianjin technical team. We return complete 2D/3D CAD submittals, material datasheets, and direct factory pricing within 24 hours.