
Featured Industrial Valve Assemblies & Disc Integration
Discover our precision-machined discs mounted in fully certified industrial valve assemblies, verified for municipal distribution, chemical plants, fire protection, and subsea pipelines.
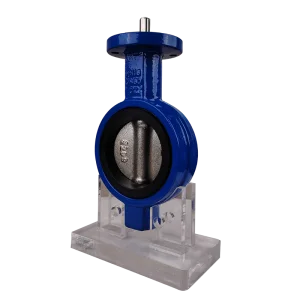
OEM Earless Wafer Type Butterfly Valve
Configure Valve Disc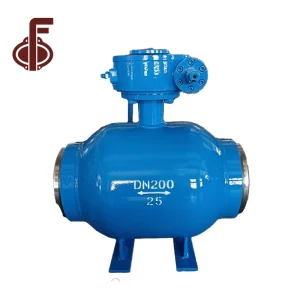
China Fully WELDED STEEL BALL VALVE
Configure Valve Disc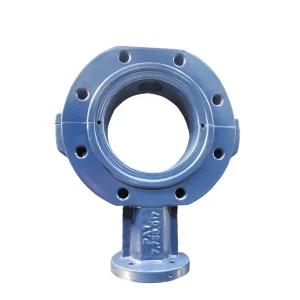
China Fully Lug Butterfly Valve Two Pieces Body
Configure Valve Disc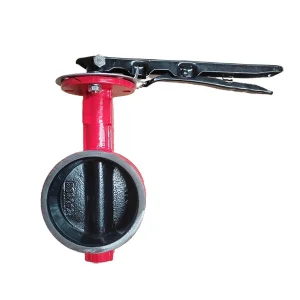
OEM Grooved Type Butterfly Valve for Fire Fighting
Configure Valve Disc
Worm Gear CF8 Disc Double Stem Wafer Valve
Configure Valve Disc
OEM Stainless Body WCB Single Disc Check Valve
Configure Valve Disc
Rubber Lined Disc Wafer Butterfly Valve
Configure Valve Disc
China Wafer Butterfly Valve Ductile Iron Body
Configure Valve DiscEngineering the Critical Flow Component: Anatomy of the Butterfly Valve Disk
The butterfly valve disk is the solitary moving boundary in direct contact with continuous, turbulent fluid momentum. As a China butterfly valve disk factory founded in 2006, Tianjin Zhongfa Valve Co., Ltd. (ZFA Valve) operates at the convergence of fluid structure interaction (FSI) analysis, precision investment casting, and nanometer-scale edge polishing.
Concentric Symmetrical Discs
Designed for resilient-seated wafer and lug valves up to PN25. Features a mirror-finished spherical sealing edge (Ra ≤ 0.4 μm) that minimizes friction torque against EPDM, NBR, and Viton elastomers, eliminating premature seat extrusion.
Double Eccentric Cam Geometry
Engineered for high-performance process lines. The shaft centerline is offset from the body bore and disc face, allowing the disc to cam cleanly out of the seat within the first 5 degrees of stroke, virtually mitigating local seat rubbing.
Triple Offset Conical Profile
Machined via multi-axis CNC to create an inclined conical profile. Generates frictionless, pure rotary wedging contact with metal-to-metal laminated graphite or solid Stellite seals, delivering Class VI bubble-tight sealing from -196°C up to +600°C.
Metallurgy & Encapsulation: Resisting Cavitation, Abrasion, and Chloride Stress
A butterfly valve disk is subject to cavitation implosion, differential pressure loading, and aggressive electrochemical attack. Our foundry facilities utilize vacuum degassed casting and specialized encapsulation technologies tailored to exact chemical media.
| Alloy / Coating System | International Standard Spec | Tensile / Yield Strength (MPa) | Target Media Compatibility | Erosion / Corrosion Resistance |
|---|---|---|---|---|
| Austenitic Stainless (CF8M / SS316) | ASTM A351 / EN 10213 1.4408 | ≥ 485 / ≥ 205 | Organic acids, potable water, HVAC, light corrosive chemical lines | PREN 23-25 High pitting resistance |
| Super Duplex (2507 / UNS S32750) | ASTM A890 Grade 5A / CE3MN | ≥ 750 / ≥ 550 | SWRO seawater desalination, offshore brine, bleaching plant chemicals | PREN ≥ 42 Immune to chloride cracking |
| Nickel Aluminum Bronze (C95800) | ASTM B148 / UNS C95800 | ≥ 585 / ≥ 240 | Marine ballast, fire mains, marine biofouling environments | Exceptional bio-growth and erosion resistance |
| Hastelloy C276 (CW-12MW) | ASTM A494 / UNS N10276 | ≥ 690 / ≥ 310 | Wet chlorine gas, hypochlorite, flue gas desulfurization (FGD) scrubbers | Extreme oxidizing & reducing acid resistance |
| Ductile Iron + Nylon 11 (Rilsan) | ASTM A536 65-45-12 / GGG40 | ≥ 450 / ≥ 310 | Potable drinking water, demineralized water, municipal pipelines | Fluidized-bed 300-500 μm impact-resistant barrier |
| Fully Encapsulated PTFE / PFA | ASTM D4894 Virgin Polymer Core | Dielectric Breakdown ≥ 20 kV | Ultra-pure chemicals, concentrated sulfuric acid, semiconductor DI water | Isostatically molded ≥ 3.0 mm non-porous sheath |
China Factory 4.0: Supply Chain Resilience, Automation & Scale
Operating from our automated foundry and machining workshops in Tianjin, ZFA Valve couples the industrial strength of Northern China's metallurgy cluster with high-speed 5-axis robotic CNC cells to supply Tier-1 EPC contractors and OEM valve assemblers worldwide.
Direct Chemical Traceability
Real-time optical emission spectrometry (OES) conducts multi-point metallurgical melt verification before pouring, guaranteeing EN 10204 3.1 chemical and mechanical compliance on all heats.
Robotic 5-Axis CNC Profiling
Eliminates human indexing inaccuracies. Dual-stem broaching, spline milling, and double/triple offset conical sealing curves are turned in a single clamping with spatial tolerances under ±0.008 mm.
Rigorous NDT Matrix
Zero structural internal voids. 100% radiographic inspection (RT) and liquid penetrant testing (PT) across the hub-to-disc transition zone, where torsional fluid shear stress peaks under emergency closure.
Logistics & Port Proximity
Located minutes from Tianjin Port (Xingang), our containerized export workflow secures streamlined customs clearance, sea-freight vapor barrier crating, and fast 14-day production turnarounds on standard disc patterns.
Engineered Solutions Across High-Reliability Critical Sectors
From hyper-saline brine circulation to municipal potable water distribution, our discs deliver low hydrodynamic torque coefficients ($C_{td}$) and optimize overall pipeline energy efficiency.
Desalination & Seawater SWRO
Raw seawater and high-pressure brine rapidly pit conventional stainless steels. We manufacture disc components from Super Duplex 2507 and Nickel Aluminum Bronze (C95800) with passivated finishes, mitigating crevice corrosion beneath elastomeric liner lips.
Power Generation & FGD Scrubbers
Coal and biomass flue gas cleaning combines high sulfurous slurry with elevated operating temperatures. Our Hastelloy C276 and 1.4529 alloy discs withstand pH drops down to 1.5 while resisting abrasive fly-ash particulate scouring.
Municipal Water & District HVAC
Large-diameter ductile iron discs (up to DN3000) encapsulated in food-grade WRAS/NSF-61 approved epoxy or Nylon 11 provide hydrodynamic profiling, reducing pressure drops by up to 22% compared to blunt planar casting designs.
Global Procurement Matrix: Specifying Discs for Minimum Lifecycle Cost
Plant availability depends on valve reliability. Choosing the cheapest cast disc frequently introduces porosity, erratic breakaway torque, and seat blowout. Leading international procurement teams evaluate disc tenders using standardized technical parameters.
Actuator Sizing & Dynamic Torque
A hydrodynamic contoured disc profile reduces fluid dynamic torque peaks at 60°–75° open positions. This allows engineers to downsize pneumatic or electric actuators by one frame size, cutting automation CAPEX by 15%–30%.
Pinless vs. Pinned Disc Connections
ZFA Valve delivers both through-bolted pinned connections and internal double-D/square spline drive systems. Our pinless designs eliminate potential leak paths and galvanic corrosion between mismatched shaft and taper pin materials.
Cavitation Index ($K_c$) Optimization
When operating under high pressure drop throttling, our CFD-optimized airfoil disc edges control vortex shedding, delaying cavitation onset and shielding adjacent downstream piping from vibration-induced acoustic fatigue.
Audited Quality Management & Multi-Standard Compliance
Global engineering procurement requires verifiable proof of compliance. Tianjin Zhongfa Valve operates an ISO 9001:2015 quality framework with CE-PED European pressure equipment certification.
ISO 9001:2015 Registered
Complete batch tracking from incoming ingots to sand reclamation, core manufacturing, mold filling, annealing, and final dispatch crating.
CE-PED 2014/68/EU
Certified for pressure containment integrity within Category III Module H conformity criteria, enabling frictionless distribution across the European Economic Area.
Global Flange Standards
Fully compatible with ASME B16.5 Class 150/300, EN 1092-1 PN10/PN16/PN25, JIS B2220 10K/16K, and AS 2129 Table D/E bolt pitch circles.
Full MTR Documentation Pack
Every shipment includes complete EN 10204 3.1 inspection certificates, hydrostatic shell test charts, liquid penetrant reports, and positive material identification (PMI) logs.
Technical Roadmap & Future Outlook: Toward Zero-Defect Additive Manufacturing
As industrial processes become more severe, traditional sand castings are evolving. ZFA Valve invests in advanced manufacturing technologies to extend service life in extreme environments.
3D Sand Printing & Topology Optimization
Binder-jet 3D sand printing creates internally ribbed, lightweight hollow discs. This cuts rotational mass and actuator torque by up to 35% without sacrificing pressure containment under water hammer conditions.
Directed Energy Deposition (DED) Stellite
Laser-cladded cobalt-base hardfacing on triple eccentric disc cones creates metallurgical bonds with zero micro-cracking and ultra-low dilution, replacing manual TIG welding for dependable 600°C service.
Smart Discs with Acoustic Erosion Sensing
Currently developing pilot disc stems with wireless strain and acoustic-emission transducers. These monitor cavitation-induced micro-jets and disc flutter in real time, enabling predictive maintenance before catastrophic seal leakage.
Frequently Asked Engineering & Sourcing Questions
Clear technical answers to the most common questions raised by EPC piping engineers, procurement directors, and valve repair facilities.
What metallurgical criteria distinguish CF8, CF8M, and CF3M butterfly valve discs?
CF8 corresponds to cast AISI 304 stainless steel containing 18% Cr and 8% Ni, serving clean water, air, and mild oxidizing environments. CF8M incorporates 2.0%–3.0% Molybdenum, which raises the Pitting Resistance Equivalent Number (PREN) above 23 to guard against localized chloride pitting. CF3M is the extra-low-carbon variation (maximum 0.03% C vs 0.08% in CF8M). CF3M prevents chromium carbide precipitation at grain boundaries during post-weld cool-down or high-temperature service, avoiding intergranular corrosion in chemical processing pipelines.
Why is dynamic torque critical when designing large-diameter butterfly valve discs?
Dynamic torque ($T_{dyn}$) arises from asymmetric fluid pressure distributions acting on the leading and trailing halves of an open disc. At angles between 60° and 80°, hydrodynamic lift creates severe closing torque. In designs over DN600, dynamic torque can easily surpass seating friction torque. Our engineering team utilizes cambered hydro-profile disc designs to equalize boundary-layer pressure drop across the wings, lowering dynamic torque peaks by up to 25% and preventing actuator stalling.
How do pinned vs. pinless disc-to-stem connections compare under cyclic loading?
Pinned connections utilize taper pins driven perpendicularly through the disc hub and shaft. While mechanically reliable for static on/off systems, cyclic throttling can loosen the pins over time, introducing hysteresis and creating galvanic corrosion cells between mismatched pin and shaft alloys. Pinless configurations drive the disc through internal close-tolerance double-D flats, internal splines, or square drives completely sealed from line media. This eliminates through-disc leak paths, simplifies seat replacements, and provides longer fatigue life under modulating control.
What surface treatment is recommended for ductile iron discs in municipal drinking water lines?
Ductile iron discs (ASTM A536 65-45-12 / GGG40) should receive electrostatic fluidized-bed Nylon 11 (polyamide) or fusion-bonded epoxy (FBE) encapsulation with a minimum dry film thickness of 250–400 μm. Nylon 11 is preferred because its low water absorption, exceptional impact resistance, and low surface energy resist scaling. It also lowers seat seating torque while complying with international sanitary standards including WRAS, NSF/ANSI 61, and ACS.
What quality control protocols prevent porosity and shrinkage voids in valve disc castings?
At ZFA Valve, disc molds are engineered using 3D MAGMA casting flow and solidification simulation software to optimize riser placement and chill design, eliminating hot spots. Every heat undergoes vacuum degassing, optical spectrometry analysis, and microstructural verification. Finished rough castings receive 100% liquid penetrant testing (PT) along sealing perimeters and high-stress hub fillets, supplemented by radiographic examination (RT) conforming to ASME B16.34 Section 8 on critical project heats.
Can ZFA Valve manufacture custom replacement discs for third-party valve maintenance?
Yes. As a full-capability China butterfly valve disc manufacturer, our reverse engineering workshop utilizes FaroArm 3D laser coordinate scanning to capture worn disc geometries, stem hole broaching dimensions, and seat profiles with ±0.015 mm precision. We can reproduce and machine drop-in replacement discs in high-grade alloys (such as Duplex 2205 or C95800) for aging or obsolete valve bodies within 10 to 18 business days.
Explore Related Engineered Valve Series & Critical Spare Parts
ZFA Valve supplies complete engineered valve systems alongside OEM replacement disc components to water utility concessions, chemical processing plants, marine shipyards, and mechanical contractors worldwide.
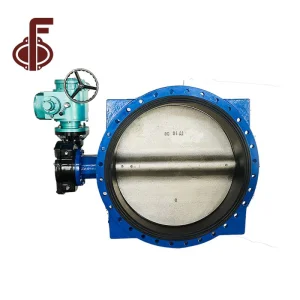
Large Diameter Electric Flange Butterfly Valve
Configure Valve Disc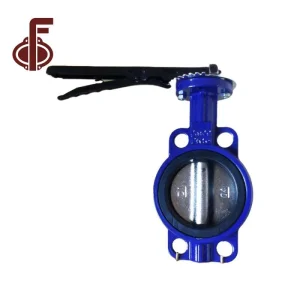
OEM ZA01 Ductile Iron Wafer Butterfly Valve
Configure Valve Disc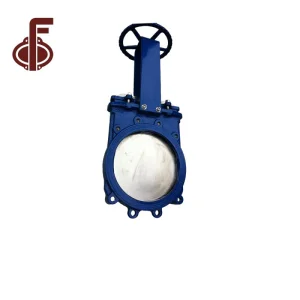
OEM DI PN10/16 Class150 Lug Knife Gate Valve
Configure Valve Disc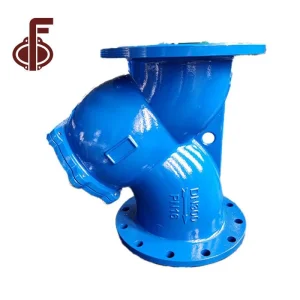
China DI CI SS304 Flange Y Strainer
Configure Valve Disc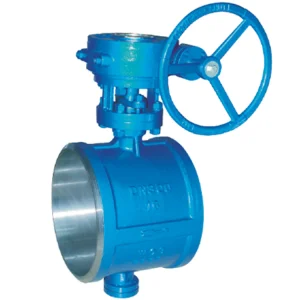
OEM Butt Welded Triple Offset Butterfly Valve
Configure Valve Disc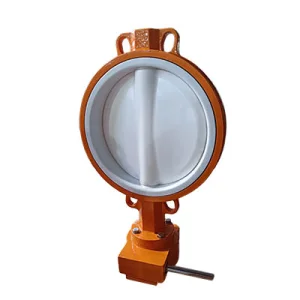
PTFE Lined Disc & Seat Wafer Butterfly Valve
Configure Valve Disc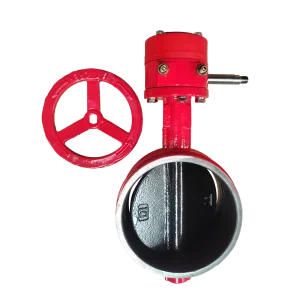
Grooved Butterfly Valve Fire Signal Remote Control
Configure Valve Disc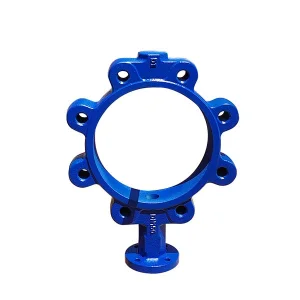
OEM Butterfly Valve Lug Body for Sea Water
Configure Valve DiscNeed Custom Butterfly Valve Discs or OEM Production Tooling?
Our engineering team in Tianjin reviews your drawings, CFD parameters, alloy specifications, and dimensional standards within 24 hours. Contact our technical department directly for certified quotation packages.
