Factory Direct Precision Valves & High-Torque Gear Actuation
Explore heavy-duty butterfly and industrial gate valves manufactured for municipal waterworks, HVAC district loops, hydrocarbon transport, and aggressive chemical processing plants.
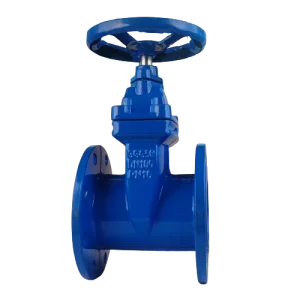
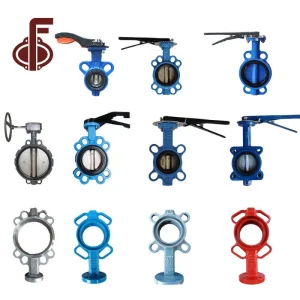
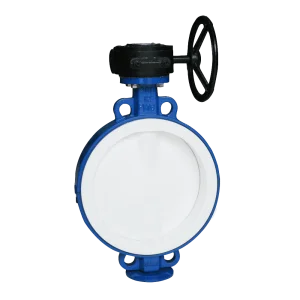
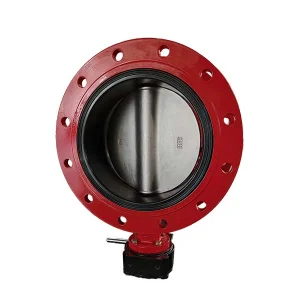
Engineering Principles of Butterfly Valves with Worm Gear Operators
In high-pressure and large-bore flow regimes, fluid dynamic torque renders direct manual lever actuation ergonomically unfeasible. Worm gear manual actuators provide mechanical advantage, precision throttling, and intrinsic hydraulic stability.
Self-Locking Kinetic Drive
Worm gearboxes utilize high-precision helical bronze or ductile iron gears driven by hardened alloy steel worms. The low lead angle provides irreversible mechanical self-locking, preventing media line surges from forcing the disc out of position.
- Eliminates hazardous fluid back-torque
- Prevents destructive hydraulic water hammer
- Guarantees repeatable quarter-turn micro-positioning
ISO 5211 Standardized Top Flange
Manufactured strictly with standardized ISO 5211 mounting pads and keyed or double-D stem profiles. This enables interchangeability between manual worm gear units, multi-turn electric actuators, and pneumatic scotch-yoke drives.
- Enclosure ratings certified to IP65 / IP67 / IP68
- Adjustable travel limit mechanical stops (±5°)
- Clear visual yellow/red open-close dial indicators
Low-Rim-Pull Ergonomics
Compliant with international ergonomics standards (such as EN 12570), input handwheel diameter and gear ratio are matched to ensure the manual rim pull effort remains below 250 N even under maximum differential shut-off pressure.
- Reduces operator fatigue on large pipelines
- Dual-stage spur/planetary gearboxes for >DN600
- Lockable handwheels for field safety lockout-tagout (LOTO)
Engineering Torque Calculation Breakdown
Total operational valve torque (Ttotal) is computed via: Ttotal = Tseat + Thydrostatic + Tbearing + Tpacking. While lever handles are physically restricted to low torque applications (<300 Nm, typically DN50–DN150), worm gears multiply operator effort by ratios ranging from 24:1 up to 720:1, allowing smooth regulation across bore diameters exceeding DN2000 under full rated differential pressure (ΔP).
China Factory Cluster Advantages in Valve Manufacturing
Operating out of Tianjin—China's foremost valve manufacturing and deep-water export logistics hub—Tianjin Zhongfa Valve integrates specialized raw casting foundries, automated precision CNC machining, and comprehensive metallurgical testing.
Foundry Metallurgical Control
Direct ownership of induction melting and resin-bonded sand casting facilities ensures tight chemistry control of ductile iron (GGG40 / GGG50 / QT450-10) with nodularity over 90%, preventing micro-porosity and brittle failures.
Cost-to-Quality Optimization
By coupling localized supply chains for raw pig iron, elastomer compounding, and gearbox housings with streamlined high-throughput CNC machining, China offers a 30% to 45% total cost of ownership advantage for EPC projects.
Rapid Prototype to Mass Production
From CAD drawing review to initial 3D tooling molds, sample machining, and hydrostatic pressure qualification, our in-house engineering team accelerates standard OEM cycles from 12 weeks down to 20 business days.
Tianjin Deep-Water Logistics Hub
Strategically situated near Xingang Port (Tianjin), our facility offers direct maritime shipping lanes worldwide, reducing domestic drayage risks, cutting customs transit overhead, and ensuring on-time delivery of crated valves.
Global Enterprise Technical Specification Matrix
Selecting the proper elastomeric liner, disc metallurgy, and body casing geometry is critical to avoiding premature seat degradation, galvanic corrosion, and stem seal blowouts in critical process pipelines.
| Seat Material | Hardness & Temperature | Ideal Flow Media | Fluid Incompatibilities | Applicable Standards |
|---|---|---|---|---|
| EPDM (Ethylene Propylene) | Shore A 70±5 -20°C to +120°C |
Potable drinking water, municipal wastewater, seawater, low-pressure steam, HVAC condenser lines | Hydrocarbon solvents, mineral oils, concentrated aromatic acids, aromatic fuels | EN 681-1, WRAS, DVGW, FDA 21 CFR |
| NBR / Buna-N (Nitrile) | Shore A 75±5 -15°C to +85°C |
Crude oil, diesel fuel, lubricating oils, kerosene, hydraulic fluids, compressed natural gas | Ozone, direct UV exposure, methyl ethyl ketone (MEK), phosphate esters, strong oxidizers | ASTM D2000, ISO 4633, API 609 |
| PTFE / PFA (Fluoropolymer) | Shore D 55±5 -25°C to +180°C |
Concentrated sulfuric/hydrochloric acids, chlorine gas, pharma solutions, high-purity chemicals | Liquid fluorine, molten alkali metals, severe high-velocity slurry abrasive particles | FDA 177.1550, USP Class VI, ISO 5208 |
| FKM / Viton (Fluoroelastomer) | Shore A 75±5 -15°C to +200°C |
Hot petroleum fuels, aggressive solvents, synthetic engine lubricants, chemical refining lines | Low-molecular organic acids, anhydrous ammonia, polar solvents (acetone, esters) | MIL-R-83248, ISO 1629 |
| Metal-to-Metal (Stellite / SS316) | Hardfaced Alloy -196°C to +550°C |
Superheated steam, thermal oil, hot flue gases, abrasive refining catalysts, cryogenic LNG | Subject to tight particulate filtering requirements to prevent wire-drawing leakage | API 607 Fire Safe, ISO 10497 |
Valve Body Configuration Guidance: Wafer vs. Lug vs. Double Flanged
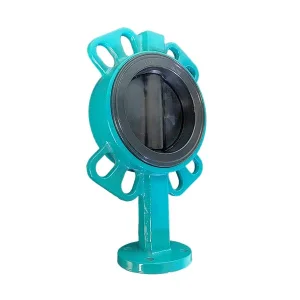
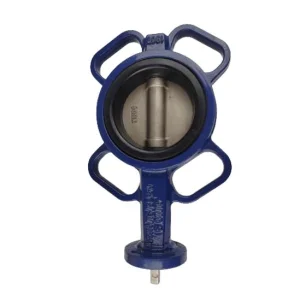
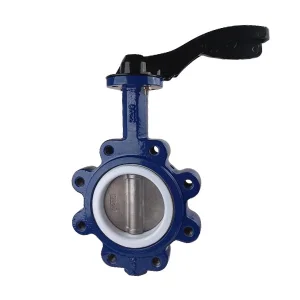
Wafer Style: The most compact, lightweight, and cost-effective layout. Installed sandwiched between pipeline flanges using continuous long all-thread studs. Ideal for enclosed skids and HVAC where weight reduction is prioritized. Note: Not rated for downstream dead-end service.
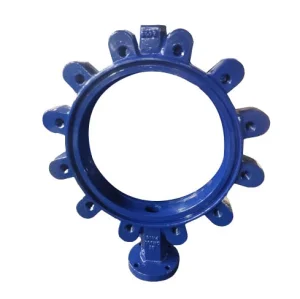
Lug Style: Features drilled and tapped threaded lugs matching flange bolt circles. Permits removal of downstream piping while maintaining full upstream line pressure (dead-end isolation). Mandatory for pump discharge manifolds and marine ballast compartments.
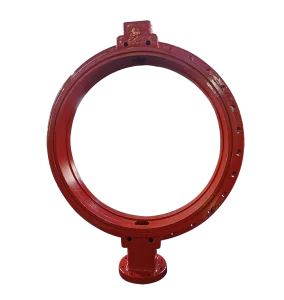
Double Flanged Style: Heavy-duty dual integral flange design engineered for large diameters (DN600 up to DN2400) and subterranean water transmission lines. Provides maximum mechanical rigidity against pipeline bending moments.
Regulatory Compliance, Inspection & Factory Traceability
ZFA Valve implements zero-defect quality policies compliant with European, North American, and Eurasian industrial pressure standards, ensuring smooth site acceptance for EPC engineers and safety auditors.
Pressure Equipment Directive (PED) & CE
Certified in compliance with EU Directive 2014/68/EU Module H. Complete documentation dossiers include EN 10204 3.1 Material Test Reports (MTRs), chemical spectral analysis, tensile testing, and Charpy impact verifications.
- Full traceability from melt heat numbers to machined stems
- Hydrostatic shell test at 1.5× nominal working pressure
- Resilient seat closure test at 1.1× rated ΔP (Rate A zero-leak)
Advanced NDT & Coating Integrity
Valves receive non-destructive testing including magnetic particle inspection on castings, ultrasonic wall thickness scans, and liquid penetrant testing on critical weld overlays and pinless shaft connections.
- Electrostatic epoxy coating ≥250µm (AkzoNobel/Jotun)
- High-voltage holiday spark testing (zero micro-pinholes)
- Salt spray resistance tested >1000 hours per ASTM B117
Multi-Standard Drilling Compatibility
Custom machining allows multi-standard bolt patterns matching ASME/ANSI B16.1 Class 125, B16.5 Class 150, EN 1092-2 PN10/PN16/PN25, JIS B2239 10K/16K, AS 2129 Table E, and GOST 12820 on a single valve body.
- Eliminates warehouse stock proliferation
- Streamlines field replacements across global sites
- Precision CNC back-spot facing for uniform bolt torquing
Localized Industrial Use Cases & Operating Environments
From seawater reverse osmosis plants in the Arabian Gulf to district heating grids across Eastern Europe, worm gear butterfly valves deliver long-term isolation reliability.
Water Supply & Desalination
Large-bore double-flanged butterfly valves installed in SWRO intake pumping systems. Equipped with nickel-aluminum bronze (C95800) or 2507 super duplex discs to withstand aggressive chloride pitting and cavitation damage.
HVAC & Central District Cooling
Concentric wafer valves fitted with food-grade EPDM liners. Worm gear actuators enable balancing and flow throttling on chillers, cooling towers, and heat exchangers without hydraulic vibration or seat fluttering.
Chemical & Semiconductor Lines
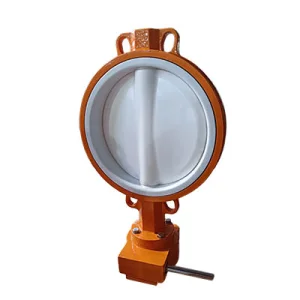
Fully fluoropolymer lined valves featuring virgin PTFE/PFA minimum 3mm body liners and encapsulated stainless steel discs. Eliminates metallic contamination in wet-etch acids, caustic soda, and high-purity solvents.
Marine & Offshore Ballast Systems
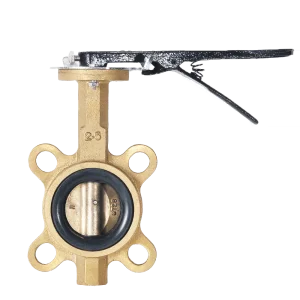
Compact ductile iron or bronze lug-type butterfly valves with IP68 waterproof gearboxes designed for continuous submerged operation in cargo vessel ballast manifolds, bilge discharge, and fuel transfer skids.
Trends Shaping the Industrial Butterfly Valve Industry
Modern process automation, environmental mandates, and digital twins are transforming manual valve engineering from basic mechanical assemblies into intelligent, low-emission flow assets.
Smart IoT Worm Gearboxes
Integration of wireless low-power magnetic angle encoders and load cells directly into manual worm gear housings. Provides SCADA systems with real-time disc position feedback and operational torque monitoring to detect seat scale buildup before valve seizure occurs.
ISO 15848-1 Low Fugitive Emissions
Global net-zero regulations demand near-zero greenhouse and VOC leakage. Advanced quadruple O-ring and live-loaded chevron PTFE stem packing systems ensure stem sealing meets Class AH fugitive emission limits under thermal cycling.
CFD-Optimized Low Hydrodynamic Drag Discs
Utilizing high-performance computational fluid dynamics (CFD) to design ultra-thin, hydrofoil-contoured valve discs. By lowering the drag coefficient (Cd) and maximizing Cv values, pumping energy consumption across municipal loops is reduced by up to 14%.
Frequently Asked Questions by Valve Engineers & Procurement Teams
Direct technical answers regarding torque ratings, installation tolerances, seat material resistance, and factory testing protocols from Tianjin Zhongfa Valve Co., Ltd.
When is a worm gear actuator mandatory instead of a manual hand lever?
A worm gear operator is generally required on concentric resilient-seated butterfly valves sized DN200 (8 inches) and larger, as well as on high-performance double and triple eccentric valves starting from DN100 (4 inches). Operating manual levers on larger valves risks sudden hydraulic kickback and seat pinching due to dynamic line torque. Additionally, industrial piping codes specify that handwheel manual rim pull must not exceed 250 N (approx. 25 kgf) under peak differential pressure.
How does ZFA Valve guarantee zero-leakage shut-off under API 598 and ISO 5208?
Every single valve undergoes 100% two-stage hydrostatic and pneumatic testing prior to dispatch. The body shell is pressurized to 1.5 times the nominal working pressure (e.g., 24 bar for PN16 rating) to confirm casting structural integrity. The resilient seat is then tested to 1.1 times nominal rating (17.6 bar for PN16) with water and low-pressure air at 6 bar. ZFA resilient-seated valves adhere strictly to ISO 5208 Rate A (zero visible bubble leakage).
What is the structural difference between concentric and eccentric butterfly valves?
In concentric (rubber-lined) valves, the stem and disc centerlines align precisely with the valve bore, creating 360-degree constant contact with the elastomer seat throughout travel. In double eccentric (high performance) valves, the shaft is offset both behind the disc and off-center from the pipe axis, causing the disc to cam away from the seat upon initial opening to reduce seat friction and wear. Triple eccentric valves add a third conical seating axis, enabling non-rubbing, metal-to-metal bubble-tight sealing under extreme temperatures up to 550°C.
What documentation and test certificates are delivered with overseas shipments?
Standard documentation dossiers sent with our export orders include: EN 10204 Type 3.1 Inspection Certificates containing spectrographic chemical analysis and tensile test data; Hydrostatic and Pneumatic Factory Test Reports; Coating Thickness Inspection Logs (≥250µm DFT); CE Certificate of Conformity under PED 2014/68/EU; and ISO 9001:2015 Quality Management System documentation. Third-party inspection (SGS, BV, TÜV, Lloyd's Register) is supported upon project request.
Can worm gear operators be field-retrofitted with electric or pneumatic actuators?
Yes. All ZFA worm gear butterfly valves are designed with ISO 5211 direct-mount standardized top flanges and removable drive sleeves. To retrofit an electric or pneumatic actuator, the worm gearbox is unbolted from the top plate, leaving the stem exposed. An actuator with a matching ISO 5211 flange code (such as F07, F10, F14, or F16) and corresponding shaft keyway can then be mounted directly without pipeline depressurization or special transition brackets.
Specialized Flow Control, Knife Gate & Resilient Seated Valves
Review additional configurations including fully lined fluoropolymer valves, lever-to-gear convertibles, brass-bronze alloys, and GOST/ANSI-compliant isolation valves from our Tianjin workshops.