
High-Performance Flow Isolation & Control Products
Engineered to ASTM, ANSI, DIN, BS, and JIS standards. Discover our OEM and direct-supply stainless steel, resilient seated, and engineered gate configurations built for extreme industrial cycles.
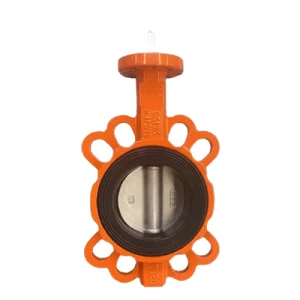
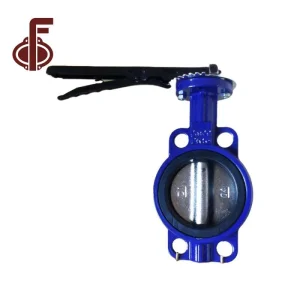
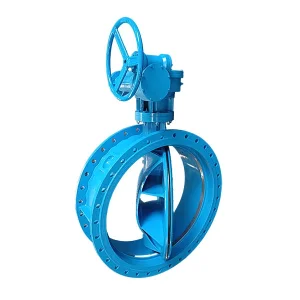
Tianjin Zhongfa Valve (ZFA Valve): Industrial Authority Since 2006
Decades of metallurgical innovation, precision CNC machining, and rigorous hydrodynamic validation solidify China’s premier position in global stainless steel quarter-turn valve manufacturing.
Two Decades of Dedicated Flow-Control Metallurgy
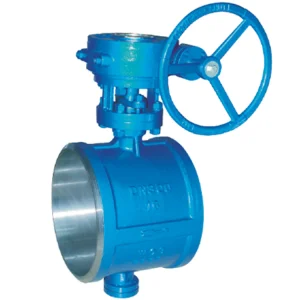
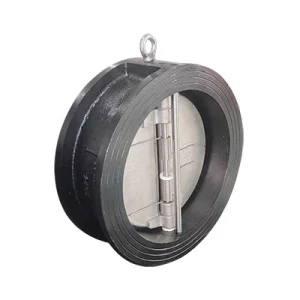
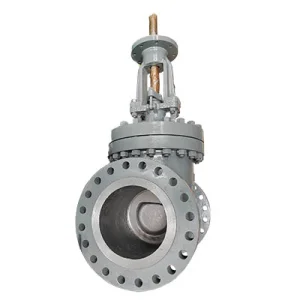
Founded in 2006, Tianjin Zhongfa Valve Co., Ltd. (ZFA Valve) operates as a tier-one manufacturing powerhouse specializing in high-integrity quarter-turn isolation and modulating valves. Our core industrial portfolio spans concentric resilient seated butterfly valves, double eccentric high-performance valves, triple offset metal-to-metal zero-leakage valves (TOV), resilient and metal-seated gate valves, dual-plate check valves, and knife gate valves engineered for demanding process lines.
Every valve casting, machined disc, ground stem, and vulcanized elastomer liner conforms to an audited ISO 9001:2015 Quality Management System and carries European CE / PED (Pressure Equipment Directive 2014/68/EU Module H) certification. By maintaining dedicated investment casting lines and sand-casting foundries in Northern China, we empower multinational engineering procurement contractors (EPCs) and OEM brand owners to achieve significant cost efficiency without sacrificing metallurgical integrity.
From pre-sale 3D computational fluid dynamics (CFD) sizing and cavitation prevention to finite element stress analysis (FEA) and post-sale technical field training, ZFA Valve delivers robust, audit-ready flow solutions built to endure aggressive, corrosive, and high-cycle industrial duties.
Executive Engineering Verification
As international flow standards evolve toward stricter carbon reduction and zero fugitive emission tolerances, sourcing directly from a vertically integrated factory ensures full material traceability from raw ingots to packaged products.
- 100% Shell and Hydrostatic Seat Proof Pressure Testing per API 598 & ISO 5208
- EN 10204 Type 3.1 Certified Raw Chemical and Mechanical Mill Test Reports (MTR)
- ISO 5211 Standardized Actuator Top Flange for Direct Coupling with Electric/Pneumatic Units
- Positive Material Identification (PMI) Spectrometry on Every Alloy Disc & Stem
Austenitic & Duplex Stainless Steel Metallurgy for Extreme Service
Selecting the precise casting grade and stem metallurgy dictates service longevity, localized pitting resistance, and structural yield in aggressive chemical, offshore, and municipal lines.
| Alloy Grade | Standard Equivalents | PREN Value | Yield Strength (MPa) | Optimal Media Environments | Incompatible Media Risks |
|---|---|---|---|---|---|
| CF8 (SS304) | ASTM A351 CF8 / 1.4308 / SUS304 | ~18.0 - 20.0 | ≥ 205 MPa | Potable water, HVAC chilled water, commercial glycol loops, neutral food slurries | High chlorides (>200 ppm), warm seawater, hot hydrochloric/sulfuric acids |
| CF8M (SS316) | ASTM A351 CF8M / 1.4408 / SUS316 | ~23.0 - 25.0 | ≥ 240 MPa | Industrial wastewater, low-salinity brines, mild organic acids, pulp bleaching liquors | Stagnant high-temperature seawater, concentrated wet chlorine gas |
| CF3M (SS316L) | ASTM A351 CF3M / 1.4404 / 316L | ~23.5 - 25.5 | ≥ 215 MPa | Biopharmaceutical WFI loops, sanitary clean steam (CIP/SIP), cryogenic LNG piping | High mechanical abrasion or extreme velocity particulate slurries |
| 2205 Duplex | ASTM A995 Gr 4A / 1.4462 / S31803 | ~34.0 - 36.0 | ≥ 450 MPa | Seawater reverse osmosis (SWRO), coastal desalination, offshore ballast systems | Continuous temperatures above 300°C due to 475°C embrittlement phenomenon |
| 2507 Super Duplex | ASTM A995 Gr 5A / 1.4410 / S32750 | ≥ 42.0 | ≥ 550 MPa | High-pressure desalination brine discharge, deepwater subsea valves, sour gas (NACE MR0175) | Non-standard cryogenic applications below -50°C without Charpy impact verification |
Corrosion Mechanism Mitigation
Crevice and pitting corrosion are prevented by maintaining strict molybdenum additions (≥2.0% in CF8M) and nitrogen control during secondary AOD refining at our Tianjin casting facilities.
Stem Torsional Integrity
Valves employ high-tensile 17-4PH (UNS S17400) precipitation-hardened or ASTM A276 Type 316 one-piece blow-out proof stems, eliminating shaft deflection under maximum shutoff differential pressure (ΔP).
Surface Electropolishing & Passivation
Castings undergo mechanical glass-bead blasting and nitric-acid chemical passivation to ASTM A967, ensuring a dense chromium-oxide passive film that withstands aggressive sterilization cycles.
Structural Configurations: Concentric vs. Double vs. Triple Offset
Understanding kinematic geometry determines operational torque, seat friction wear, cycle life, and thermal-pressure performance boundaries across industrial flow installations.
Concentric Resilient Seated
The stem center and disc center coincide exactly with the pipe centerline. Interference sealing between the spherical stainless steel disc perimeter and the vulcanized elastomer liner delivers bi-directional bubble-tight shutoff.
- Pressure Ratings: PN10, PN16, Class 150 (200 PSI)
- Body Patterns: Wafer, Lug, Flanged
- Liner Options: EPDM, NBR, Viton, PTFE boot
- Primary Advantage: Ultra-economical, zero maintenance
Double Offset (High Performance)
Offset 1 shifts the shaft behind the sealing plane; Offset 2 shifts the shaft eccentric to the pipe center. The cam action lifts the disc rapidly out of the seat within the first few degrees of rotation, drastically cutting seat scrub.
- Pressure Ratings: Class 150 / 300, PN25, PN40
- Seats: RPTFE, PEEK, Inconel energizer
- Cycle Capability: 500,000+ continuous cycles
- Application: Hydrocarbon condensate, steam lines
Triple Offset Metal-Seated (TOV)
Offset 3 introduces an inclined conical sealing axis. The disc engages the seat only at the final point of shut-off without rubbing, delivering friction-free, non-jamming metal-to-metal sealing at extreme temperatures.
- Pressure Ratings: ASME Class 150 to Class 900
- Temp Range: -196°C (Cryogenic) up to +650°C
- Leakage Class: API 598 Rate A Zero Leakage
- Safety: Inherently Fire-Safe per API 607 / ISO 10497
Why Tier-1 Chinese Stainless Steel Valve Factories Lead Global Supply
Combining the Tianjin-Hebei foundry corridor, high-speed multi-axis robotic machining centers, and an integrated supply chain yields unmatched technical precision and rapid lead times.
Direct Foundry Integration & Raw Material Control
Unlike Western assembly-only distributors, Chinese manufacturers operate direct foundry partnerships. High-frequency induction melting furnaces ensure spectral chemistry is stabilized before pouring, guaranteeing consistent disc wall thickness.
5-Axis CNC Machining & Robotic Grinding
Sealing faces, stem bores, and flange serrations are machined in single-clamping operations. Robotic super-finishing polishes stainless steel discs to Ra 0.2 μm, cutting rubber seat wear and operating torque by over 30%.
Agile Supply Chain Lead Times
By housing body casting stocks, modular disc blanks, and vulcanization presses within our Tianjin industrial hub, custom-engineered orders ship within 15–25 business days, compared to 16–24 weeks for Western manufacturers.
Global Enterprise Sourcing Demands & Lifecycle TCO Optimization
EPC contractors, international distributors, and plant maintenance engineers evaluate total cost of ownership (TCO) based on lifecycle reliability, cavitation resistance, and spare part interchangeability.
CapEx vs. OpEx Lifecycle Balance
Upgrading to CF8M or Duplex 2205 discs in water treatment or HVAC cooling towers incurs only an 8–15% CapEx premium over cast iron, while extending mean time between failures (MTBF) from 3 years to over 12 years.
Engineering QA/QC Dossiers
Tender qualification demands complete documentation. We deliver complete vendor data packages (VDP), including casting radiography (RT), dye penetrant (PT), hydrostatic pressure logs, and coating dry-film thickness (DFT) reports.
OEM Private Labeling & Spares Support
We engineer customized casting nameplates, laser body etching, customer-branded packaging, and precision replacement parts (liners, disc-stem sets, packing rings) to streamline after-market MRO inventory.
Global Certification, PED/CE Directives & Localized Technical Support
Strict adherence to regional environmental and safety regulations guarantees frictionless import customs clearance and project site commissioning worldwide.
CE / PED 2014/68/EU
Certified for Category I, II, and III piping systems under European Pressure Equipment Directives with full notified body auditing.
WRAS, NSF/ANSI 61
Potable water approved EPDM and Rilsan polyamide nylon coatings prevent microbial contamination in municipal drinking supply.
ATEX & SIL-3 Safety Loops
Explosion-proof design for hazardous explosive zones (Zone 1/21) and certified functional safety data for emergency safety instrumented systems.
FDA 21 CFR §177.2600
Virgin virgin PTFE and high-purity silicon seat materials meet strict food, beverage, and active pharmaceutical ingredient (API) criteria.
Emerging Valve Technologies: Digital Twins, Low Emissions & Clean Hydrogen
Industrial flow control is transforming rapidly. Discover how intelligent actuation, ISO 15848-1 fugitive emission containment, and cryogenic metallurgy define the future of flow engineering.
ISO 15848-1 Low Fugitive Emission Gland Packing
Stem sealing systems utilize live-loaded graphite and cup-and-cone chevron PTFE packings, slashing volatile organic compound (VOC) micro-leakage below 100 ppmv to meet worldwide ESG net-zero emission mandates.
Smart Actuation & Industrial IoT Diagnostic Feedback
Integration with intelligent electric quarter-turn actuators supporting Modbus, Profibus, and WirelessHART protocols provides real-time operating torque profiling, stroke travel alarms, and predictive valve seat maintenance.
Clean Hydrogen & Cryogenic LNG Service
Extended bonnet configurations machined from solid forged 316L keep gland packings above freezing in -196°C LNG service, while specialized surface burnishing prevents hydrogen embrittlement in clean energy storage grids.
Mission-Critical Applications for Stainless Steel Butterfly Valves
Across harsh marine environments, corrosive chemical manufacturing, and sterile hygienic facilities, our valves deliver dependable cycle isolation.
Seawater Desalination (SWRO)
Duplex 2205 disc and vulcanized EPDM wafer butterfly valves operating continuously in high-chloride intake and brine reject pipelines, demonstrating zero crevice attack after 80,000 operational hours.
Biopharmaceutical & Sterile WFI Loops
Mirror-polished CF3M (316L) butterfly valves with fully encapsulated pure PTFE split bodies, surviving daily clean-in-place (CIP) with 2% caustic wash and steam-in-place (SIP) up to 135°C without seal degradation.
Marine Ballast & Exhaust Scrubbers
Lug-type butterfly valves with CF8M discs and aluminum bronze alloy bodies, operating under DNV-GL marine standards to regulate exhaust gas recirculating washwater containing corrosive sulfuric acid residues.
Seat Polymer Chemistry & Temperature-Pressure Operating Envelopes
Seat elastomer degradation causes more than 80% of valve failures. Use our empirical engineering selection matrix to pair the liner polymer with process fluid chemistry.
| Seat Material | Hardness (Shore A) | Temperature Envelope | Compatible Process Fluids | Contraindicated Media |
|---|---|---|---|---|
| EPDM (Food Grade / Standard) | 70 ± 5 | -20°C to +120°C (-4°F to 248°F) | Potable water, wastewater, glycol, chilled water, hot water, dilute alkalis, ozone | Hydrocarbons, mineral oils, diesel fuels, concentrated aromatic acids |
| NBR (Buna-N Nitrile) | 75 ± 5 | -10°C to +82°C (14°F to 180°F) | Petroleum diesel, hydraulic oils, lubricating grease, compressed air, oily water | Ketones, polar solvents (MEK), brake fluids, hot ozone, steam |
| PTFE (Teflon Polytetrafluoroethylene) | 55 ± 5 (Shore D) | -20°C to +180°C (-4°F to 356°F) | Aggressive industrial chemicals, sulfuric/nitric acids, pure chlorine, high-purity solvents | Highly abrasive hard slurries, molten alkali metals, thermal cycling past 200°C |
| FKM (Viton Fluoroelastomer) | 75 ± 5 | -15°C to +200°C (5°F to 392°F) | High-temperature mineral acids, aromatic hydrocarbons, fuels, chlorinated solvents | Low-molecular esters, amines, anhydrous ammonia, low-temperature cold services |
| Metal-to-Metal (Stellite Overlay) | Rockwell C 38-42 | -196°C to +650°C (-320°F to 1200°F) | Superheated high-pressure steam, refinery catalytic cracking, molten sulfur, coking gas | Extremely high-viscosity crystallizing slurries causing mechanical tooth binding |
Wafer Type Body Pattern
Clamped securely between pipe flanges with long studs passing completely through. The most compact, lightweight, and cost-effective layout for general pipeline installation.
Lug Type Body Pattern
Features individually tapped threaded lugs. This design permits downstream pipe removal while keeping upstream system pressure intact for dead-end terminal isolation service.
Double Flanged Pattern
Engineered with integral flanged bolt circles on both faces. Recommended for large-diameter mains (≥DN600), high-pressure district heating, and buried municipal distribution lines.
Our Controlled 5-Stage Zero-Defect Manufacturing Workflow
From metallurgical verification through precision assembly, every production stage is recorded in an ERP-tracked quality logbook.
Drawing & Spec Review
Sales engineers review process fluid velocity, operating temperatures, and ASME/DIN bolt circles to confirm design criteria.
Cast Material Spectrometry
Spectrometric chemical analysis verifies chromium, nickel, and carbon ratios prior to raw casting machining.
CNC Machining Precision
5-axis machining centers bore stem holes, contour disc profiles, and machine serrated sealing flange surfaces.
Assembly & Pressure Test
100% of valves undergo hydrostatic shell testing (1.5x PN) and pneumatic seat tightness testing per API 598 zero-leakage standards.
Marking & Export Packing
Castings receive laser heat number markings, corrosion protection, and seaworthy wooden crating compliant with ISPM 15 standards.
Technical Guides & Valve Engineering Insights
Explore authoritative practical guidance from our senior flow design engineers and manufacturing metallurgists.
Pinned vs. Pinless Disc-to-Stem Configurations
Pinless designs feature internal polygonal drive shafts or splines, eliminating disc through-hole leak paths and minimizing galvanic corrosion in harsh seawater applications.
Read Engineering PaperPipe Connection Methodology: Flanged, Wafer, Lug & Welded
Detailed breakdown of civil pipe loadings, thermal expansion bending moments, and why butt-welded triple offset valves excel in continuous high-pressure steam distribution.
Read Engineering PaperOEM Manufacturing Capabilities: Drawing to Delivery
How international valve companies partner with ZFA Valve to produce fully certified private-labeled product lines while protecting their proprietary IP and dimensional tooling.
Read Engineering PaperFrequently Asked Questions on Stainless Steel Butterfly Valves
Detailed technical answers addressing common valve sizing, material selection, standard compliance, and OEM questions.
Which international flange connection standards do your butterfly valves fit?
What is the difference between CF8, CF8M, and forged 304/316 stainless steel?
Can your factory supply custom OEM private-label branding and casting logos?
How do you verify zero leakage in resilient seated vs. metal-seated valves?
What certifications are supplied with an export valve order?
Why should buyers specify a pinless disc design instead of taper through-pins?
Engineered Automation & Severe Duty Valve Configurations
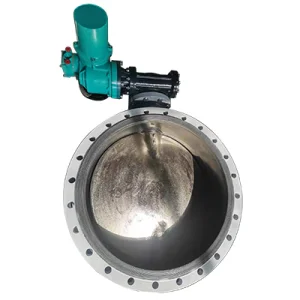
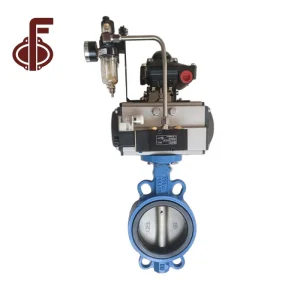
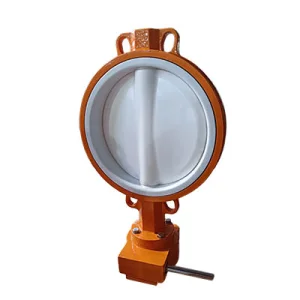
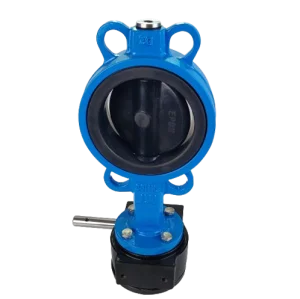
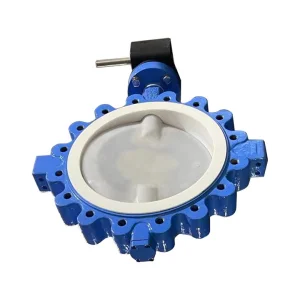
Explore pneumatic, electric, fully lined PTFE, and large-bore solutions manufactured under rigorous zero-defect quality systems.
Accelerate Your Project with Certified Valve Engineering
Connect with ZFA Valve senior application specialists for comprehensive technical datasheets, CAD 3D step files, project quotation pricing, and customized OEM development schedules within 24 hours.
