
Featured OEM Butterfly Valve Bodies & Industrial Assemblies
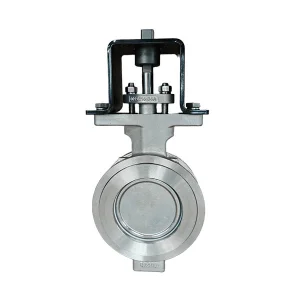
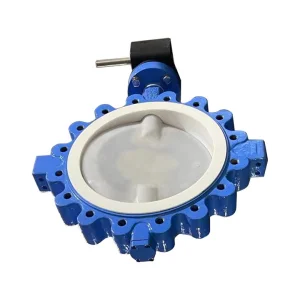
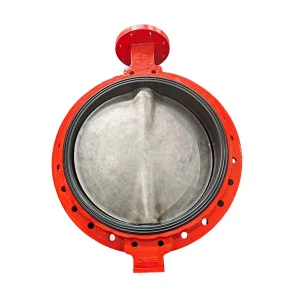
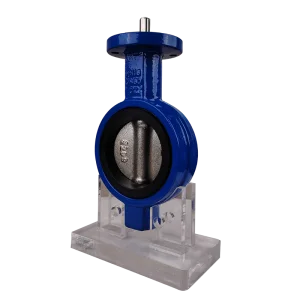
Direct factory sourcing from Tianjin Zhongfa Valve Co., Ltd. Explore our engineered split-body, wafer, lug, and double-eccentric valve body solutions built for global EPC engineering contractors and OEM valve brands.
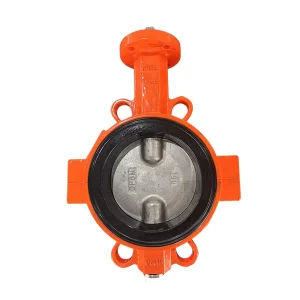
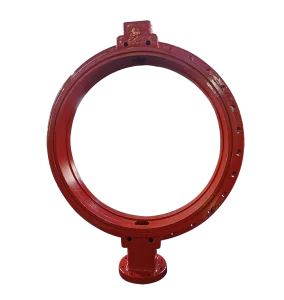
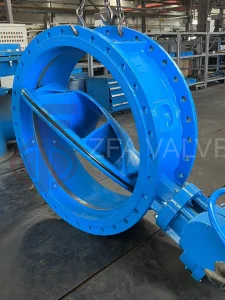
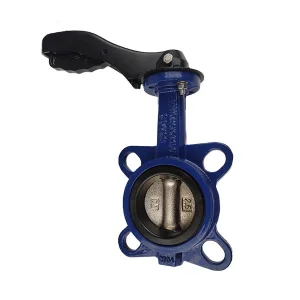
Macro Industrial Dynamics: Precision OEM Valve Body Engineering
Modern process piping demands uncompromising structural integrity. As fluid handling pressures elevate and regulatory oversight regarding fugitive emissions intensifies, valve body manufacturing stands as the primary bulwark against catastrophic pressure boundary failures.
Pressure Boundary Integrity
The valve body is the primary containment vessel resisting static line pressure, dynamic fluid hammer, and thermal pipe stresses. Under ASME B16.34 and EN 12516 calculations, OEM casting walls require precise volumetric uniformity to eliminate microporosity, shrinkage cavities, and tensile stress risers.
Sub-Micron Machining Tolerances
Seat pocket geometry and upper trunnion stem bore co-axiality govern operating torque and cycle life. ZFA Valve leverages dedicated 5-axis horizontal CNC machining centers to hold critical bore concentricity within ±0.015 mm, eliminating uneven liner compression and stem binding.
Metallurgical Traceability
Every OEM melt heat undergoes optical emission spectroscopy (OES) prior to pouring. From nodular ductile iron (ASTM A536 65-45-12 / EN-GJS-400-15) to cast carbon steel (WCB) and duplex stainless steels, chemical composition and EN 10204 3.1 certification are systematically verified.
Commercial Landscape: OEM Foundry Cost Structures & Nearshoring Strategies
Procurement teams face oscillating raw metal indices, rising freight surcharges, and stringent ESG compliance. Navigating international supply chains requires understanding foundry economics and foundry tooling models.
Total Cost of Ownership (TCO)
Direct casting cost is only 35% of true valve ownership expense. Improper body grain structures cause microscopic weeping during hydro-testing, resulting in pipeline teardown costs 20x higher than initial valve prices. ZFA's ISO 9001 quality system mitigates warranty failure rates below 0.08%.
Pattern Tooling Amortization
For custom OEM body geometries—such as specific face-to-face dimensions (ISO 5752 Series 20 vs. API 609 Table 1) or integrated mounting pads (ISO 5211 F05 through F25)—pattern cost amortization across batch quantities is critical. ZFA engineers deliver cost-neutral CNC aluminum tooling for annual contracts exceeding 5,000 units.
Tianjin Port Logistics Hub
Situated within the Northern China industrial casting corridor with streamlined access to Tianjin Xingang Port, our facility provides rapid containerized sea shipping to European main ports (Rotterdam, Hamburg), North American hubs (Long Beach, Houston), and Middle Eastern logistics channels.
OEM Butterfly Valve Body Material Metallurgy & Performance Matrix
Selecting the optimal alloy substrate prevents localized pitting, galvanic corrosion, and mechanical yield failure. The following engineering matrix cross-references standardized valve body materials manufactured in our Tianjin foundry.
| Material Designation | Tensile Strength (MPa) | Yield Strength (MPa) | Elongation (%) | Optimal Media & Industry Deployment | Thermal Operating Envelope |
|---|---|---|---|---|---|
| Ductile Iron (QT450-10 / GGG40) ASTM A536 65-45-12 |
≥ 450 | ≥ 310 | ≥ 10 | Municipal potable water, HVAC chilled/condenser loops, non-aggressive fire protection mains. | -10°C to +120°C |
| Cast Carbon Steel (WCB) ASTM A216 WCB |
≥ 485 | ≥ 250 | ≥ 22 | High-pressure district energy steam, boiler feedwater, non-corrosive hydrocarbons, refining. | -29°C to +425°C |
| Austenitic Stainless (CF8 / 304) ASTM A351 CF8 |
≥ 485 | ≥ 205 | ≥ 35 | Food & beverage, brewery lines, nitric acid service, industrial cooling water with moderate chlorides. | -196°C to +538°C |
| Acid-Resistant Stainless (CF8M / 316) ASTM A351 CF8M |
≥ 485 | ≥ 205 | ≥ 30 | Desalination brine reject, pulp & paper bleaching, chemical synthesis, sulfuric acid injection. | -196°C to +600°C |
| Nickel Aluminum Bronze ASTM B148 C95800 |
≥ 585 | ≥ 240 | ≥ 15 | Offshore platform sea-cooling, naval ballast systems, subsea riser manifolds, marine scrubbing. | -20°C to +260°C |
Resilient Seat & Liner Chemical Compatibility Guide
Seat material and end connection drive 80% of butterfly valve specification inquiries. Reference these parameters prior to finalizing your valve body datasheet.
| Seat Polymer | Typical Fluid & Process Media | Service Temperature Limits | Media to Avoid |
|---|---|---|---|
| EPDM (Hard Back / Soft) | Potable water, municipal wastewater, chilled & hot water HVAC, mild industrial alkalis. | Approx. -20 °C to +120 °C | Mineral oils, hydrocarbon solvents, aromatic fuels. |
| NBR (Nitrile) | Lubricating oils, kerosene, diesel, hydraulic fluids, LPG, raw oily water. | Approx. -10 °C to +82 °C | Ozone exposure, automotive brake fluids, concentrated ketones. |
| PTFE (Virgin / Filled) | Concentrated mineral acids, chlor-alkali, ultra-pure fluids, pharmaceutical dosing lines. | Approx. -20 °C to +180 °C | Molten alkali metals, high-velocity quartz slurry abrasion. |
End-Connection Architecture: Wafer, Lugged & Double Flanged Bodies
The structural body casing determines installation footprint, dead-end pressure containment capabilities, and plant turnaround convenience.
Wafer & Earless Bodies
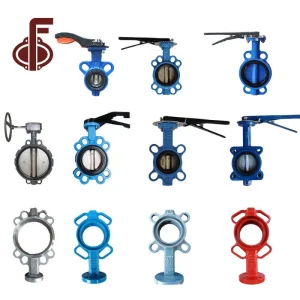
Wafer bodies clamp between two companion pipe flanges utilizing long through-bolts. This configuration features the lowest overall metal mass, minimal face-to-face dimension, and lowest weight per diameter. Perfect for tight HVAC mechanical rooms and general water distribution. (Not intended for downstream dead-end service).
Full Lugged Bodies
Featuring individually threaded bolt holes matching ANSI Class 150 or EN 1092-2 PN16 drillings. Enables independent bolt torquing from either flange face, allowing plant operators to disconnect downstream pipe spools for pump servicing while the valve maintains full rated upstream line pressure.
Double Flanged Bodies
Equipped with integral casting flanges on both ends. Delivers structural rigidity in large bore installations (DN300 to DN2400) under heavy bending moments and seismic displacements. Commonly specified in double eccentric and triple offset metal-to-metal high-temperature steam lines.
Controlled 5-Stage OEM Production & Machining Workflow
True OEM manufacturing requires full traceability from initial casting melt to finished pressure boundary inspection. Every valve body that leaves our Tianjin manufacturing complex follows this five-step quality workflow.
Senior valve designers verify pressure class (PN10/16, Class 150/300), body metallurgy, ISO 5211 top flange dimensions, and stem bore shaft tolerancing against client datasheets.
Foundry melt chemistry is verified by spectrometer. Castings undergo non-destructive ultrasonic and magnetic particle testing to ensure zero subsurface shrinkage flaws.
Flange bolt patterns, internal liner retaining pockets, and shaft journal bores are machined in single-setup horizontal machining cells to lock in true running concentricity.
Every body is subjected to hydrostatic shell testing at 1.5x nominal pressure and bidirectional seat bubble testing according to API 598 and ISO 5208 Rate A criteria.
Electrostatic epoxy powder coating is applied to a minimum 250 µm DFT thickness, followed by custom OEM tagging, protective end-caps, and fumigated export palletizing.
Global Standards, Factory Verification & Technical Certification
ZFA Valve provides certified documentation packages for tender qualification across municipal water authorisations, European PED safety directives, and American petroleum engineering mandates.

Tianjin Zhongfa Valve Co., Ltd. Audited ISO 9001:2015 & CE Certificate Pack
-
ISO 9001:2015 Management System
Rigorous quality oversight covering pattern making, sand core molding, alloy melt chemistry, CNC machining, and traceable batch stamping.
-
CE / PED 2014/68/EU Module H Conformity
Conformity verification for pressurized equipment supplied across the European Economic Area, enabling direct inclusion in engineering procurement tenders.
-
Multi-Standard Flange Matching
Precision universal flange indexing compatible with ASME B16.1 Class 125, ASME B16.5 Class 150, EN 1092-2 PN10/PN16, JIS B2220 10K/16K, and AS 2129 Table E.
Critical Field Deployments: Application-Engineered Valve Bodies
From district chilled water distribution systems to offshore desalination reverse osmosis skids, our custom butterfly valve bodies provide reliable duty cycles across extreme service profiles.
Seawater Desalination & RO
High chloride concentrations cause severe crevice corrosion in standard ductile iron bodies. ZFA supplies ASTM B148 C95800 Nickel Aluminum Bronze and duplex 2205 bodies, as well as vulcanized hard ebonite and PTFE-lined bodies that isolate wet metal surfaces from aggressive brine streams.
HVAC District Cooling & Energy
In ultra-large metropolitan district cooling complexes, pumping heads require low pressure drops to conserve megawatt-hours. Our high-flow contoured concentric wafer bodies and double-flanged butterfly valves minimize head loss while maintaining reliable bubble-tight shutoff.
Chemical & Ultrapure Dosing
Utilizing split-body two-piece designs in ductile iron or cast stainless CF8, our PTFE/PFA fully-lined series ensures zero media-to-metal contact. The engineered two-piece split body design simplifies maintenance seat cartridge replacements during scheduled plant shutdowns.
Future Outlook: Digital Twin Castings, FEA Optimization & Smart Actuation
Valve manufacturing is evolving beyond traditional green sand molding. Explore how ZFA Valve integrates computational flow dynamics, topological mass optimization, and smart IoT actuator flanges.
Topological Body FEA
By analyzing finite element stress concentrations under water-hammer spikes, our metallurgical engineers reduce non-structural dead weight by up to 14% while strengthening rib reinforcements around high-strain neck trunnions.
ISO 15848-1 Low-Emission Stems
Global carbon reduction initiatives mandate ultra-low fugitive emissions. Our refined stuffing box geometries integrate dual live-loaded chevron PTFE and graphite packing sets, certified to ISO 15848-1 Class AH / Class BH emission tight standards.
Standardized ISO 5211 Interfaces
To streamline integration with electric, pneumatic, and electro-hydraulic actuators, all ZFA valve bodies feature standardized ISO 5211 mounting flanges and precision double-D or keyed shaft drives for direct bolt-on automation without external brackets.
Frequently Asked Questions: OEM Valve Body Procurement & Engineering
Technical, manufacturing, and commercial answers for EPC project managers, procurement directors, and valve engineering teams.
Which international flange and pressure standards do ZFA butterfly valve bodies satisfy?
What certifications and quality documentation are supplied with each OEM valve order?
Can ZFA develop custom foundry patterns and OEM branded body castings?
How do engineers choose between pinned and pinless disc-to-stem connections?
What is the standard turnaround time for technical inquiries and custom casting quotes?
Full Industrial Valve & Component Directory
Quick access to our specialized flow-control configurations and replacement parts lines.
Engineered Industrial Valves, Gate Valves & Actuation Assemblies
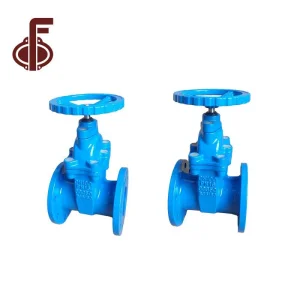
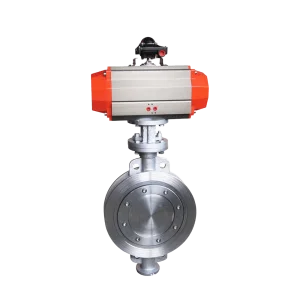
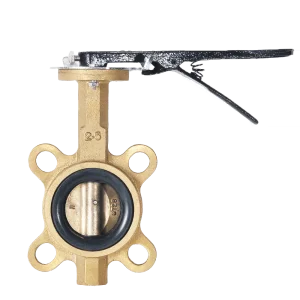
Browse our precision engineered triple eccentric metal-seated valves, brass-bronze alloys, high performance double-eccentric configurations, and ductile iron gate valves manufactured for global supply.
Request Full Valve Technical Catalogs & Foundry Quotations
Partner directly with Tianjin Zhongfa Valve Co., Ltd. for factory-direct butterfly valve body castings, complete automated assemblies, and customized flow equipment. Our senior engineering team reviews datasheets, provides 3D CAD models, and quotes project bills of materials within 24 hours.