Featured Industrial Valve & Stem Assemblies
Direct supply of certified concentric, eccentric, and industrial pipeline flow solutions designed for severe services and standard OEM assemblies.
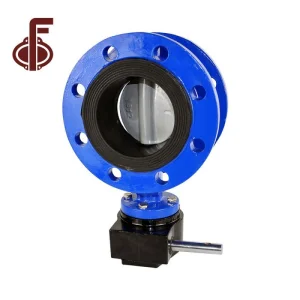
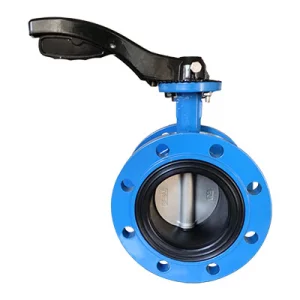
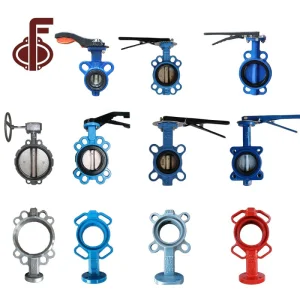
China Ductile Iron Body Worm Gear Flange Type Butterfly Valve Manufacturers, Exporters
View Specifications →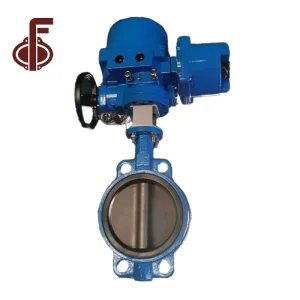
Engineering Integrity: Critical Torque Transmission & Sealing Dynamics
The valve stem (or shaft) represents the primary mechanical lifeline of any quarter-turn quarter-stroke assembly. In butterfly valves, the stem must deliver frictionless actuation, zero torsional deflection, and comprehensive blowout prevention under cyclic hydrostatic stresses.
Torsional Strength & Shear Load
Under tight line shutoffs, dynamic differential pressures create extreme resisting torque on the butterfly disc. Our stems are engineered using precipitation-hardened alloys (17-4PH) and high-grade ferritic-martensitic steels (SS410, SS420) to guarantee safety margins exceeding 2.5x the peak breakaway torque.
Integral Blowout-Proof Retention
In full alignment with ASME B16.34 and API 609, OEM stems feature integral stepped shoulders or high-tensile retaining snap-rings situated within the valve bonnet. This configuration ensures that line media pressure cannot eject the stem even during gland packing maintenance under active pressure.
Single-Shaft vs. Two-Piece Shaft
We produce both through-shaft designs for maximum alignment rigidity in heavy-duty slurry lines, and stub-shaft (two-piece) configurations that streamline fluid flow through the valve disc center, cutting overall pipeline pressure drop (higher Cv ratings) by up to 18%.
OEM Metallurgy Matrix: Stem Materials Selection for Corrosive Lines
Matching stem metallurgy to process media prevents galvanic pitting, stress-corrosion cracking (SCC), and thermal binding across aggressive municipal and industrial flow systems.
| Material Grade | Yield Strength (MPa) | Hardness (HBW/HRC) | Ideal Application Environment | International Standard Equiv. |
|---|---|---|---|---|
| SS410 / SS420 | ≥ 450 - 550 | 200 - 240 HBW | Non-corrosive water, HVAC, general building utilities, mild hydrocarbons. | ASTM A276 Type 410 / 420; EN 1.4006 |
| SS304 / SS316 | ≥ 205 - 240 | ≤ 217 HBW | Desalination pre-treatment, food & beverage, municipal wastewater, mild organic acids. | ASTM A276 Type 304 / 316; EN 1.4401 |
| 17-4PH (SUS630) | ≥ 725 - 850 | 28 - 35 HRC | High-pressure shutoff, offshore skids, petrochemical refining, high-cycle automation. | ASTM A564 Grade 630; UNS S17400 |
| Duplex 2205 / Super Duplex | ≥ 450 - 550 | ≤ 32 HRC | Brine discharge, high-chloride chemical lines, marine ballast water treatment. | ASTM A276 S31803 / S32750; EN 1.4462 |
| Monel K-500 / Hastelloy C276 | ≥ 690 - 790 | 27 - 38 HRC | Sour gas (NACE MR0175), pure chlorinated environments, geothermal steam lines. | UNS N05500 / UNS N10276 |
China Factory Supply Chain Ecosystem: Scale, Speed & Total Cost Advantage
How our centralized manufacturing base in Tianjin delivers unmatched supply predictability, raw material stability, and rapid turnaround for worldwide valve brands and infrastructure contractors.
Full-Spectrum Cluster Integration
Our hub integrates induction smelting, hot-forging mills, and multi-axis CNC machining within an 80-kilometer radius. This vertical consolidation slashes material lead times, dampens global raw alloy price spikes, and allows standard stem production cycles within 10 to 15 working days.
Sub-Micron CNC Finishing
Valve stems undergo centerless cylindrical grinding and automatic burnishing to achieve surface roughness below Ra 0.2 to Ra 0.4 μm in the packing gland interface. This ultra-smooth boundary reduces friction against PTFE and graphite packing sets, cutting fugitive emissions.
Complete Heat Treatment Traceability
Every batch of forgings undergoes computer-monitored solution annealing, quenching, and tempering. We guarantee full chemical and mechanical lot integrity backed by EN 10204 3.1 Mill Test Certificates (MTC) verifying yield, elongation, and Charpy V-notch impact performance.
Meeting Global Procurement Demands: OEM Specifications & Interfaces
Addressing the complex engineering challenges of international EPC procurement agents, OEM brand managers, and plant maintenance directors.
Actuation Drive Adaptation (ISO 5211)
Seamless automation compatibility is achieved through precision-milled double-D drives, square keys, parallel keys, or involute splines conforming strictly to ISO 5211 flange mounting dimensions. This ensures zero play during quarter-turn motorized or pneumatic operation.
Pinned vs. Pinless Disc Interlocking
We supply stems for conventional taper-pin lockouts and modern polygon/splined pinless assemblies. Pinless stem connections isolate the shaft completely from the process fluid, eliminating leak pathways through disc pin holes and allowing easier seat replacements in field revamps.
Bespoke Shaft Lengths for Thermal Ext.
For cryogenic liquefaction processes (-196°C) or superheated steam circuits (+450°C), our OEM workshop fabricates extended valve stems. These allow proper insulation clearance and keep the actuator assembly at safe ambient temperatures.
Localized Support & Global Compliance Assurance
Ensuring cross-border compliance across North America, the European Union, the Middle East, and Asia-Pacific industrial corridors.
Pressure Equipment Directive (PED/CE)
Full conformance with the European Union PED 2014/68/EU Module H. All valve stems supplied to European distributors meet essential safety requirements, hydrostatic burst calculations, and material ductility thresholds.
Fugitive Emission Control (ISO 15848-1)
With global industrial decarbonization mandates intensifying, our stems are ground to precise micron tolerances, verified against ISO 15848-1 and API 641 to prevent volatile organic chemical (VOC) leakage down to Class AH levels.
Potable Water Safety Verifications
For municipal drinking water installations, our finished parts are prepared free from toxic lubricants and heavy metal contaminations, aligning with NSF/ANSI 61, WRAS, and DVGW potable health thresholds.
Industry Trends & Critical Application Environments
From smart automated water grids to ultra-pure semiconductor fluid handling, high-performance butterfly valve stems enable reliable operations across vital global infrastructure.
Municipal Desalination & Seawater RO
Seawater reverse osmosis demands resistance to severe crevice attack. Our Super Duplex 2507 and Duplex 2205 stems operate continuously in high-chloride intake environments without mechanical degradation.
District Heating & HVAC Energy Grids
Continuous thermal cycling can cause binding in unmachined stems. Our specialized thermal relief geometry ensures smooth quarter-turn modulation across central heating and high-rise commercial chillers.
Automated Process & Smart Valves
Modern plants demand high-frequency positioning with minimal hysteresis. By utilizing precision-broached keyways and hardened 17-4PH shafts, we ensure immediate actuator response for smart IoT automated networks.
Frequently Asked Questions (FAQ) for Valve Engineers & Buyers
Expert answers addressing stem tolerances, material validation, customization, and export logistics.
What stem tolerances and surface finishes do you achieve on OEM butterfly valve shafts?
Our Tianjin machining center holds CNC diameter tolerances within ±0.005 mm (ISO h7 to h9 fit). The stem packing contact zone is micro-ground and burnished to Ra ≤ 0.4 μm (down to Ra 0.2 μm on request), significantly lowering operating friction, extending elastomeric/PTFE packing longevity, and meeting strict fugitive emission standards.
How do you verify stem material integrity and prevent mechanical fatigue failure?
All raw bar stock undergoes 100% Ultrasonic Testing (UT) per ASTM A388 to detect internal voids, micro-fissures, and inclusions. We run tensile, yield, Charpy impact, and hardness testing on every heat-treated lot, providing complete EN 10204 3.1 certification and spectral Positive Material Identification (PMI) prior to packing.
Can you manufacture stems customized to existing valve body and disc designs?
Yes. As a genuine OEM manufacturer, we produce stems according to client CAD drawings (SolidWorks, AutoCAD, STEP files) or reverse-engineer physical samples. Customizations include special spline teeth, custom keyways, non-standard double-D flats, and extended lengths for cryogenic or elevated-temperature bonnets.
What is the difference between single-shaft and two-piece (stub) shaft construction?
A single through-shaft traverses the entire disc, offering maximum deflection resistance in severe high-pressure drops. A two-piece (stub-shaft) configuration features upper and lower stems leaving the disc center unobstructed, which increases hydrodynamic flow efficiency, maximizes the flow coefficient (Cv), and decreases overall system pumping energy.
What lead times and minimum order quantities (MOQ) apply for OEM export contracts?
For standard stainless steel grades (SS410, SS304, SS316), prototype and trial lots can be machined within 7 to 10 days, while container volumes typically ship within 20 to 30 days. We maintain flexible MOQ policies to support valve maintenance workshops, brand OEM assembly lines, and EPC project spare parts packages.
Complementary OEM Valve Series & Pipeline Hardware
Explore our complete export range of multi-standard butterfly valves, cast steel gate valves, ball valves, and replacement components.
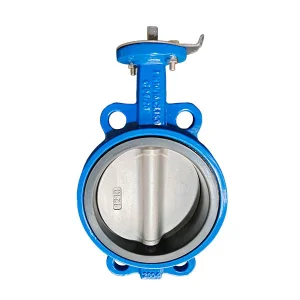
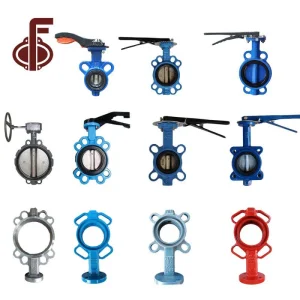
OEM Universal Wafer Butterfly Valve Compatible with PN10, PN16, ASME Class 150 and JIS 10K Manufacturers, Factories
View Specifications →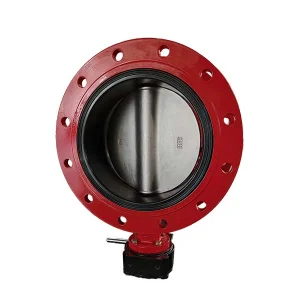
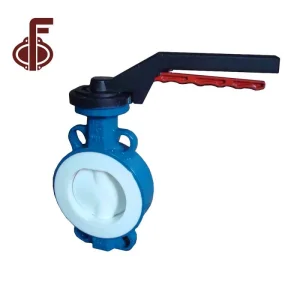
OEM Two Shaft Replaceable Seat Double Flange Butterfly Valve Manufacturers, Exporter
View Specifications →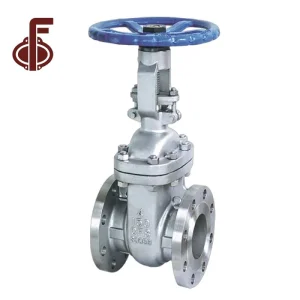
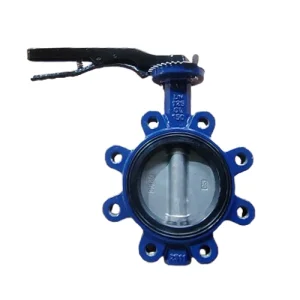
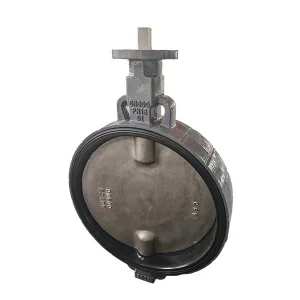
OEM CF8M Disc Dovetail Seat Lug Butterfly Valve CL150 Manufacturers, Exporters
View Specifications →