
Featured Full Bore & Industrial Valve Series (Part I)
Explore our project-grade, zero-pressure-drop, bi-directional sealing solutions built strictly to ASME B16.34, API, and EN specifications.
-
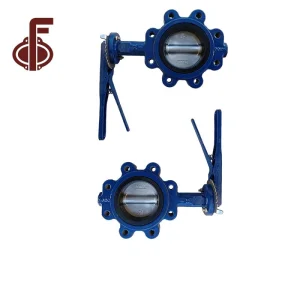
China Ductile Iron SS304 Disc Lug Type Butterfly Valves
Configure Specs -
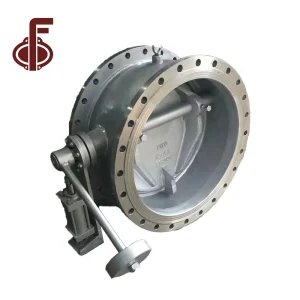
OEM Butterfly Check Valve with Heavy Hammer Manufacturers
Configure Specs -
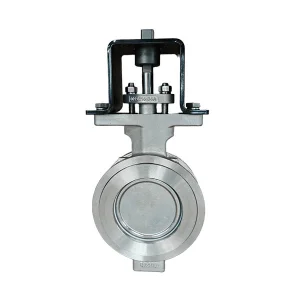
China CF8 Wafer High Performance Butterfly Valve with Support
Configure Specs -
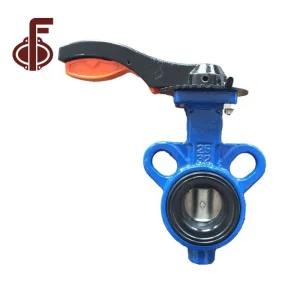
OEM Wafer Type Butterfly Valve with Aluminum Handle
Configure Specs -
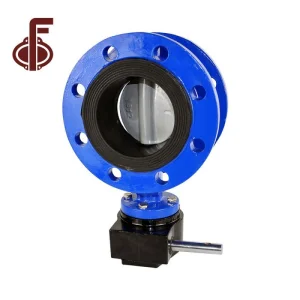
China Ductile Iron Body Worm Gear Flange Type Butterfly Valve
Configure Specs -
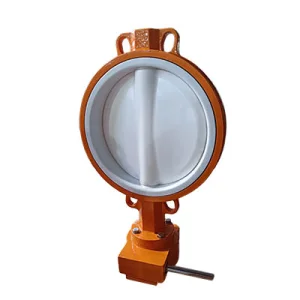
China PTFE Lined Disc & Seat Wafer Butterfly Valve
Configure Specs -
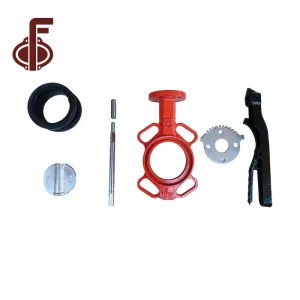
OEM Replaceable Seat Aluminum Hand Lever Wafer Valve
Configure Specs -
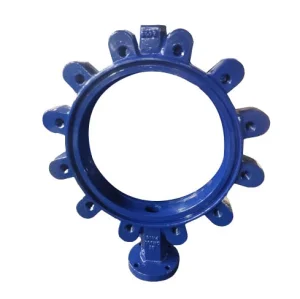
OEM Butterfly Valve Fully Lug Body Manufacturers, Exporter
Configure Specs
The Full Bore Paradigm: Global Sourcing & Pipeline Fluid Mechanics
Evaluating hydrodynamic efficiency, mechanical piggability, and fugitive emission liabilities across multinational industrial installations.
Hydraulic Continuity & Full Port Fluid Dynamics
In midstream pipeline systems and critical refinery loops, flow restriction is direct capital waste. Standard reduced bore valves impose hydraulic drag, generating boundary-layer vortices and static pressure drops. Full bore (full port) gate valves feature an internal diameter strictly congruent with the mating pipe schedule (matching ASME B36.10M / B36.19M).
- Maximizes flow coefficient (Cv value) to system theoretical maximum
- Eliminates localized turbulence, erosive impingement, and vibration
- Enables unrestricted passage for intelligent pigging, scrapers, and cleaning tools
Stem Sealing Integrity & Fugitive Emission Risk
With global environmental mandates enforcing strict penalties for volatile organic compounds (VOC) and methane leaks, mechanical seal integrity is non-negotiable. Modern full bore gate valves engineered in China incorporate certified Low-E multi-ring die-formed flexible graphite stem packing rings with braided anti-extrusion end-rings.
- Third-party certified to API 622, API 624, and ISO 15848-1 Class AH
- Self-aligning two-piece packing gland prevents stem scoring during high cycles
- Integral back-seat mechanical isolation allows on-line repacking under pressure
Wedge Architecture & Thermal Binding Mitigation
Severe thermal cycling in high-pressure steam networks and hydrocarbon refining triggers differential expansion between valve bodies and closure members. Solid wedge designs often seize due to thermal binding or mechanical seat distortion caused by bending moments in heavy pipeline runs.
- Precision engineered flexible wedge designs accommodate structural pipeline deflection
- Through-conduit slab gate and expanding gate mechanisms ensure bi-directional bubble-tight shutoff
- Stellite Gr. 6 and Gr. 21 PTA weld overlays eliminate galling at temperatures up to 538°C
Critical EPC Procurement Advisory: Minimum Wall Thickness Compliance
A prevalent pitfall in global gate valve sourcing involves non-compliant wall thickness variations between ASME B16.34 Standard Class and API 600 Heavy Wall requirements. Tianjin Zhongfa Valve (ZFA Valve) manufactures heavy-duty API 600 cast steel gate valves with cast wall thicknesses that strictly exceed minimum corrosion allowance rules, guaranteeing prolonged operational lifespan under severe cyclonic erosive media and sour service (NACE MR0175/ISO 15156).
Macro-Industry Solutions: Deploying Gate Valves in Harsh Environments
From offshore deepwater processing to extreme cryogenic terminals and district heating networks, configure our valves to eliminate operational downtime.
Upstream & Midstream Hydrocarbon Pipelines
Transmission pipelines transporting dry gas, wet gas, and sour crude require valves that resist particulate erosion and deliver 100% full port bore for pipeline scraper and inline inspection (ILI) tool passage.
ZFA Engineering Architecture: API 6D full bore slab gate valves and through-conduit gate valves featuring double block and bleed (DBB) capabilities, secondary sealant injection fittings for stems and seats, and fire-safe testing certified to API 607 / ISO 10497.
Petrochemical Refineries & Delayed Coking Units
Coking, hydrocracking, and catalytic reforming subject valves to operational temperatures exceeding 450°C, abrasive catalyst fines, and polythionic acid stress corrosion cracking.
ZFA Engineering Architecture: Heavy-wall ASTM A217 WC6, WC9, and C12A alloy bodies fitted with integral hardfaced Stellite 6 trim (API Trim 5), steam purges, flexible wedges, and fully guided wedge travel to prevent side thrust and chatter during high-velocity throttling transitions.
Supercritical Steam & Power Generation
High-energy piping lines in combined cycle gas turbine (CCGT) plants and coal-fired supercritical boilers operate under pressures reaching ASME Class 2500 and 4500, rendering conventional bolted bonnets prone to gasket failure.
ZFA Engineering Architecture: Pressure-seal bonnet gate valves with forged metallic sealing rings where internal line pressure acts upwardly on the bonnet, exponentially intensifying sealing load as line pressure rises.
Desalination & Seawater Reverse Osmosis (SWRO)
High-pressure seawater feed headers require total resistance to pitting and crevice corrosion under high chloride concentrations exceeding 35,000 ppm TDS.
ZFA Engineering Architecture: Super Duplex Stainless Steel (UNS S32750 / 2507, 1A/4A/5A castings) gate and butterfly valves with zero iron contamination, tested per ASTM G48 Method A for pitting corrosion resistance.
Municipal Potable Water & Wastewater Treatment
Potable water transmission grids prioritize bi-directional drop-tight sealing, zero contamination, and maintenance-free underground buried installation.
ZFA Engineering Architecture: AWWA C509 / C515 and EN 1171 resilient seated full bore gate valves. Ductile iron GGG50/QT450 bodies encapsulated completely in WRAS- and NSF/ANSI 61-approved fusion-bonded epoxy (FBE ≥ 250 μm) with vulcanized EPDM rubber wedges.
Flue Gas Desulfurization (FGD) & Slurry Mining
Gypsum slurry, fly ash disposal, and tailings transport pipelines experience severe abrasive wear that destroys conventional metallic seating within months.
ZFA Engineering Architecture: Bidirectional knife gate valves and through-conduit gate valves featuring field-replaceable heavy elastomer perimeter sleeves and bevel-edged stainless steel gates designed to slice clean through dense solids.
| Design Specification | Standards Compliance | Pressure Class / Ratings | Body Material Options | Primary Industrial Sector |
|---|---|---|---|---|
| Cast Steel API 600 Gate Valve | API 600, ASME B16.34, ISO 10434 | Class 150 to Class 2500 (PN20 - PN420) | ASTM A216 WCB, A217 WC6/WC9, A351 CF8M | Oil & Gas Refining, Petrochemical Plants |
| Through-Conduit Slab Gate Valve | API 6D, ISO 14313, ASME B16.34 | Class 150 to Class 1500 (Full Piggable) | ASTM A216 WCB/WCC, A352 LCC, Forged A105 | Cross-Country Hydrocarbon Transmission Lines |
| Pressure-Seal Bonnet Gate Valve | ASME B16.34, IBR, BS 1414 | Class 900 to Class 4500 (High Temperature) | ASTM A217 WC9, C12A, forged F22, F91 | Supercritical Fossil & Nuclear Steam Circuits |
| Resilient Seated Gate Valve | AWWA C509, AWWA C515, EN 1171 | Class 125, Class 150, PN10, PN16, PN25 | Ductile Iron EN-GJS-500-7 (GGG50), QT450 | Municipal Potable Water & Wastewater Treatment |
| Cryogenic Extended Bonnet Gate Valve | BS 6364, ASME B16.34, MSS SP-134 | Class 150 to Class 600 (-196°C to +80°C) | ASTM A351 CF8, CF8M, CF3M (Low Carbon) | LNG Liquefaction, Cryogenic Liquid Oxygen/Nitrogen |
Engineering Roadmap: Computational Fluid Dynamics & Precision Metallurgy
How advanced digital engineering, robotic hardfacing, and finite element stress analysis eliminate field failures before metal is poured.
Finite Element Analysis (FEA)
Each casting geometry undergoes rigorous 3D stress modeling under maximum differential pressure, pipeline thermal moments, and seismic loads to prevent bonnet distortion and binding.
CFD Flow Optimization
Bore contours and seat transitions are mathematically mapped via Computational Fluid Dynamics to guarantee streamlined laminar fluid movement with minimal boundary shear stress.
Plasma Transferred Arc (PTA)
Automated robotic PTA cladding deposits pore-free Stellite alloys onto seat rings and wedge facings with minimal dilution, delivering unmatched hardness (≥ 38 HRC) and wear life.
Non-Destructive Testing (NDT)
Castings are inspected in-house via 100% RT (Radiographic Testing) at high-stress junctions, UT (Ultrasonic Testing), MT (Magnetic Particle), and PT (Liquid Penetrant) per ASME Section V.
Metallurgical Integrity: The NACE MR0175 / ISO 15156 Mandate
In upstream hydrocarbon extraction, hydrogen sulfide (H2S) induced sulfide stress cracking (SSC) and stress corrosion cracking (SCC) represent catastrophic liabilities. Tianjin Zhongfa Valve mandates that all forged and cast pressure-containing parts specified for sour service strictly comply with NACE MR0175: maximum Rockwell hardness controlled beneath 22 HRC, heat treatment via quenching and tempering or normalizing, and full chemical analysis verifying strict carbon equivalent limits (CE ≤ 0.43).
Global Commercial Dynamics: Direct China Manufacturing vs. Western Tier-1 Resellers
Strategic lifecycle cost analysis (LCC) and total cost of ownership (TCO) benchmarks for international procurement teams.
35% - 48% Direct CAPEX Optimization
Bypassing multi-tier European and American commercial distributors allows project developers and EPC contractors to acquire API- and CE-certified full bore valves directly from primary manufacturing facilities in Tianjin, drastically compressing total capital expenditure without compromising testing stringency or material certs.
Integrated Industrial Cluster Velocity
Tianjin's advanced valve industrial cluster integrates automated sand casting foundries, 5-axis CNC machining centers, elastomer vulcanization plants, and accredited hydrostatic pressure testing laboratories within a 40-kilometer radius, accelerating production lead times by 3 to 6 weeks compared to fragmented western supply chains.
Dual-Traceability Certification Packs
Every shipment is accompanied by complete inspection document packs compliant with EN 10204 3.1 and independent third-party 3.2 inspection agencies (DNV, Lloyd's Register, TÜV SÜD, SGS), including chemical composition spectrometry, mechanical Charpy V-notch impact data, and API 598 pressure charts.
Engineering Economics: Total Cost of Ownership (TCO) Calculation for Isolation Valves
Global engineering directors assess valve procurement through lifecycle cost formulas:
LCC = CAPEX (Initial Cost) + C_energy (Pumping Cavitation Loss) + C_maintenance (Packing/Seat Renewal) + C_downtime (Premature Failure) - Residual Value
By implementing ZFA Valve's precision-machined full bore gate valves, pumping energy consumption is minimized through frictionless full port internal geometry ($C_v$ maximization), reducing annual pumping station kilowatt-hour consumption by up to 4.2% across long-distance distribution trunklines compared to standard reduced port alternatives.
Localization Support, Testing Protocols & Regulatory Compliance
Auditable verification protocols guaranteeing full transparency from raw melt chemistry to containerized export dispatch.
Comprehensive API 598 & ISO 5208 Pressure Testing
Every single valve undergoes high-pressure hydrostatic shell testing (1.5x nominal rating), high-pressure hydrostatic seat testing (1.1x nominal rating), and low-pressure pneumatic seat testing (80 psig air test) to verify 100% zero-leakage Rate A performance before leaving the workshop.
Live Virtual Factory Acceptance Tests (FAT)
To eliminate international travel costs for overseas EPC clients, ZFA Valve provides multi-angle HD live-streamed FAT sessions. Clients witness dimensional checks, Positive Material Identification (PMI XRF analysis), pressure gauge hold times, and torque measurements in real time.
Multilingual Engineering Documentation
We supply full submittal packages tailored for global tenders: 2D general assembly AutoCAD drawings, 3D STEP models for BIM integration, comprehensive installation & operation manuals (IOM), and bilingual documentation certified by our licensed valve engineering team.
Frequently Asked Questions by International Engineering & Procurement Teams
In-depth technical answers addressing flow hydraulics, wedge mechanics, fugitive emissions, and procurement compliance.
What distinguishes an API 600 full bore gate valve from standard ASME B16.34 gate valves?
How does full bore design prevent pigging tool damage in pipeline transmission?
What causes thermal binding in gate valves and how does flexible wedge design resolve it?
What are the key metallurgical criteria for gate valves handling sour gas (H2S)?
When should an engineer specify an OS&Y (Outside Screw and Yoke) versus an NRS (Non-Rising Stem) design?
How does ZFA Valve guarantee zero fugitive emissions under API 624 / ISO 15848-1?
What is the standard procedure for EN 10204 3.2 third-party inspection for overseas orders?
Can large-diameter full bore gate valves be installed in horizontal pipelines?
Featured Full Bore & Industrial Valve Series (Part II)
Continuous supply of high-performance check, gate, and butterfly valves built for harsh marine, fire safety, and abrasive process duties.
-
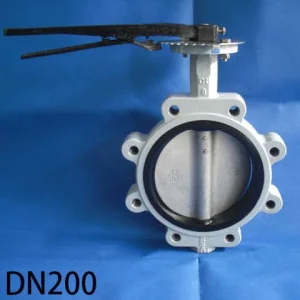
OEM Casting Iron Body CF8 Disc Lug Type Butterfly Valve
Configure Specs -
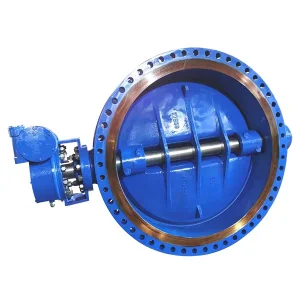
OEM Short Pattern U Shape Double Eccentric Butterfly Valve
Configure Specs -
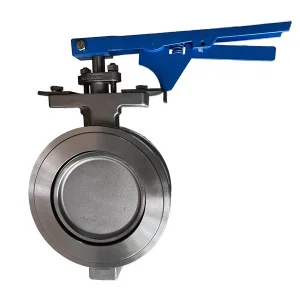
OEM Lever OP Wafer High Performance Butterfly Valve
Configure Specs -
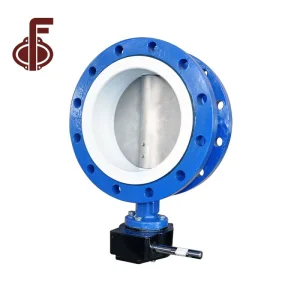
OEM PTFE Seat Flange Type Butterfly Valve Manufacturers
Configure Specs -
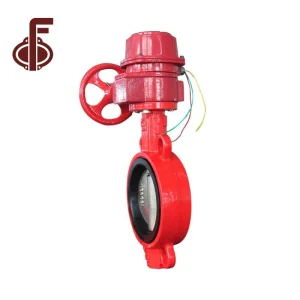
China Wafer Type Fire Signal Butterfly Valve Factory
Configure Specs -
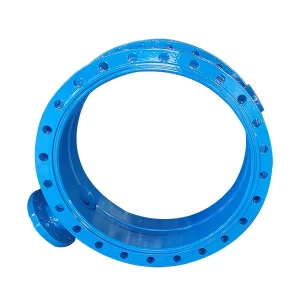
OEM Double Flanged Butterfly Body for Replaceable Seat
Configure Specs -
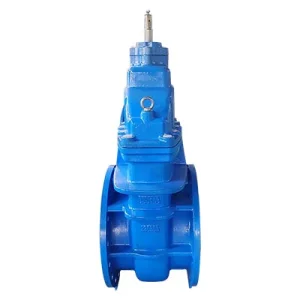
China Stainless Steel Seal Non Rising Stem Gate Valve
Configure Specs -
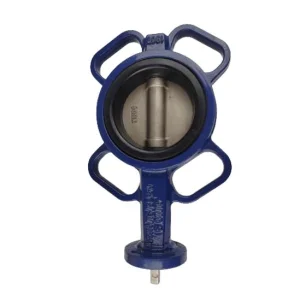
China DN80 PN10/PN16 Ductile Iron Wafer Butterfly Valve
Configure Specs
Initiate Your Engineering Consultation or Tender Bid
Connect with our senior metallurgical and mechanical application engineers in Tianjin. Submit your valve datasheets, piping schedules, and required compliance frameworks for quotation and engineering review within 24 hours.
