
Featured OEM Rubber-Seated Valve Solutions
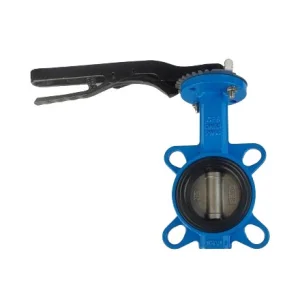
Industrial resilient seat butterfly valves, customized wafer assemblies, and pneumatic configurations precision-cast for potable water, petrochemical handling, and industrial HVAC distribution.
Global Procurement Demands for Rubber-Seated Butterfly Valves
Navigating the complex interplay of vulcanized elastomeric performance, total lifecycle cost reduction, and stringent cross-border mechanical conformance across international markets.
Severe Cycling & Durability
Global EPC contractors and municipal water operators increasingly mandate resilient seats capable of withstanding upwards of 50,000 continuous full-stroke operational cycles without loss of bubble-tight shutoff (ANSI/FCI 70-2 Class VI). Specifying custom rubber geometries eliminates liner cold-flow, prevents stem-journal blowout, and minimizes torque hysteresis under fluctuating dynamic pressure regimes.
- Elimination of elastomeric relaxation via phenolic or aluminum hard-backing
- Bi-directional sealing capability up to 16/25 Bar working pressures
- Zero pin-slip and zero stem-disc play via spline or dual-D mechanical keyways
Supply Chain Consolidation
Tier-1 procurement directors require single-source manufacturing partners who handle downstream processes completely in-house. By integrating green-sand and precision investment casting, automated multi-axis CNC disc profiling, proprietary rubber injection molding, and computerized hydro-testing, OEM valve buyers compress logistics lead times by over 35% while preserving traceability.
- Full traceability from raw melt heat chemistry to finished seat batches
- EN 10204 Type 3.1 Material Test Reports (MTRs) delivered as standard
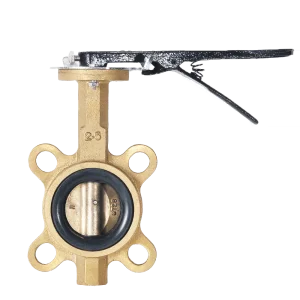
- Scalable casting runs across ductile iron (GGG40/GGG50), WCB, and Al-Bronze
Actuation-Ready Modularity
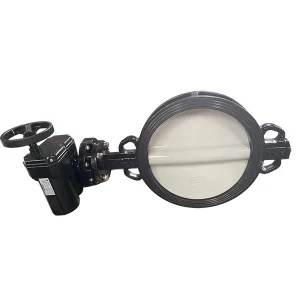
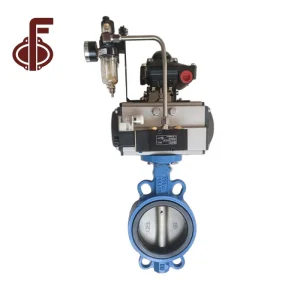
Contemporary industrial plants demand seamless integration with IoT building management systems (BMS) and SCADA loops. Concentric butterfly valves feature precision-machined ISO 5211 direct-mount top flanges, allowing instant pairing with rack-and-pinion pneumatic actuators, intelligent multi-turn electric motors, or secondary worm gear operators without costly adapter plates.
- Direct ISO 5211 top-flange configurations for backlash-free torque transfer
- Standardized stem top dimensions supporting square, keyed, and flat designs
- Low hydrodynamic resistance disc geometry lowering actuation footprint
Macro Industry Solutions & Elastomer Specification Guide
Detailed performance parameters correlating rubber compound kinetics, chemical resistance profiles, thermal bounds, and engineering standards for enterprise purchasing units.
| Seat Compound | Operating Temp Range | Optimal Service Media | Standard Compatibility | Corrosion & Wear Profile |
|---|---|---|---|---|
|
EPDM (High-Density) Ethylene Propylene |
-25°C to +135°C (-13°F to 275°F) | Potable drinking water, municipal sewage, sea water cooling, chilled water HVAC, glycol loops. | WRAS, NSF/ANSI 61, FDA 21 CFR 177.2600 | Exceptional resistance to ozone aging, dielectric degradation, weather stress; poor resistance to aromatic hydrocarbons. |
|
NBR (Buna-N) Nitrile Elastomer |
-15°C to +90°C (5°F to 194°F) | Mineral oils, hydraulic fluids, compressed air with oil mist, petroleum fuels, oily wastewater. | EN 549, ISO 6502, ASTM D2000 standard | Superior tensile strength and mechanical tear resistance against particulate slurries; degraded by halogenated solvents. |
|
FKM (Viton®) Fluoroelastomer |
-10°C to +200°C (14°F to 392°F) | Aggressive hydrocarbons, high-octane fuels, aromatic fuels, dilute acids, chemical transmission. | ISO 1043-1, API 609 Cat. A, CE-PED | Outstanding chemical resistance at extreme temperatures; limited flexibility at sub-zero temperatures. |
|
PTFE over Rubber Fluoropolymer Composite |
-30°C to +180°C (-22°F to 356°F) | Ultra-pure chemicals, active pharmaceutical processing, bio-fermentation, concentrated caustics. | FDA, USP Class VI, EC 1935/2004 | Chemically inert virgin fluoropolymer backed by resilient EPDM or silicone energizer cushions for total hermetic sealing. |
Technology Roadmap: Next-Gen Sealing & Digital Valve Twins
Bridging physical casting methodologies with Industry 4.0 predictive diagnostics, nano-engineered vulcanization, and advanced sustainability compliance.
Nano-Enhanced Elastomers
By introducing functionalized carbon nanotubes and graphene nanoplatelets into base EPDM and NBR rubber blends, molecular elasticity improves by 28%. This breakthrough prevents permanent set during extended non-cycling shutdowns and lowers operational seating torque by 15%, reducing the physical size of required pneumatic and electric actuators.
- Reduced Friction: Integrated microscopic dry-lubricants eliminate chatter
- Thermal Stability: Eliminates hardening under sustained 120°C conditions
RFID & Digital Valve Twins
Each OEM body casting can be specified with an integrated cavity for industrial passive RFID chips and laser-etched 2D data-matrix codes. Technicians in the field can access foundry melt certifications, batch seat compound vulcanization dates, installation torque values, and maintenance histories instantly through intrinsically safe mobile diagnostics.
- Zero Manual Error: Complete digitization of site inventory logs
- SCADA Handshake: Instant compatibility cross-checking during commissioning
Environmental Decarbonization
Global manufacturing benchmarks enforce low-VOC electrostatic powder epoxy coating (min. 250 μm thick) that protects cast iron and carbon steel surfaces against atmospheric corrosion while removing volatile organic compounds. Furthermore, foundry furnaces utilize closed-loop induction smelting to curb carbon intensity per finished metric ton of valve iron.
- WRAS Approved Powders: Certified for human drinking water systems
- 100% Recyclable Shells: Circular scrap metal management practices
Localized Support & Global Compliance Framework
Ensuring frictionless delivery and rigorous regulatory compliance for multinational distribution channels, regional OEM partners, and engineering consultancies.
Multi-Standard Drilling
Eliminate inventory fragmentation with multi-standard flange bolt patterns. OEM bodies are cast and machined to effortlessly slide between ASME Class 150, EN 1092-2 PN10/PN16, JIS 10K, and AS 2129 Table E mating piping, reducing distributor stock requirements by over 40%.
Private Labeling & Packaging
Custom OEM orders include customized pattern lettering (relief-cast brand logos), custom nameplates (stainless steel 304/316 with customer barcoding), bespoke corporate RAL color coatings, and heavy-duty, heat-treated fumigated marine plywood cases tailored for port transit.
Testing Verification Packs
Every shipment is accompanied by comprehensive quality assurance documentation: hydrostatic shell proof testing at 1.5× PN, bi-directional pneumatic seat leakage testing at 1.1× PN (ISO 5208 Rate A / zero bubbles), non-destructive testing (NDT/UT/MT), and coating thickness validation logs.
Complementary Heavy-Duty Isolation & Flow Valves
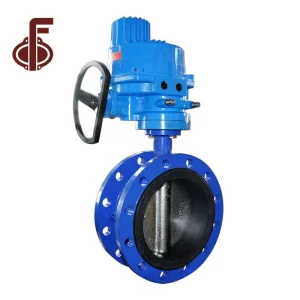
Broaden pipeline infrastructure integrity with our heavy-bore butterfly systems, rising-stem soft-sealing gate valves, and high-integrity welded ball valves.
Frequently Asked Questions (FAQ)
In-depth responses addressing technical specification challenges, custom OEM capabilities, and elastomer selection criteria.
What engineering distinctions set bonded-seat butterfly valves apart from replaceable loose-liner designs?
Bonded-seat butterfly valves feature an elastomer vulcanized directly onto the valve body casting or a rigid phenolic/aluminum cartridge back-ring. This construction prevents seat wrinkling, distortion, and displacement under high-velocity turbulent flow and full vacuum conditions (down to 0.01 bar absolute). Conversely, loose replaceable boot-liners offer quick on-site refurbishment for low-pressure municipal applications, lowering maintenance costs over decades of standard water distribution.
How does our foundry prevent disc-to-stem corrosion and galvanic reaction?
We address galvanic and crevice corrosion through precision metallurgical matching. For seawater and demineralized line environments, we combine high-strength duplex stainless steel (2205/2507) or nickel-aluminum bronze (C95800) discs with 17-4PH precipitation-hardened monel or stainless stems. In pinless disc configurations, the fluid medium is completely isolated from the shaft by internal O-rings and interference-fit rubber sleeves, eliminating wetted galvanic couples altogether.
What is the minimum batch requirement and tooling lead time for custom OEM casting designs?
As a true OEM manufacturer, our production line handles customized mold engineering efficiently. 3D solid pattern modeling and CNC wooden/aluminum tooling typically take 15 to 25 business days. Prototype sample pours, machining, vulcanization, and CMM dimension verification require an additional 10 days. Minimum order quantities (MOQs) depend on the valve bore: large diameter valves (DN600–DN1200) require no minimum batch, while standard commercial sizes (DN50–DN300) generally start at 50–100 pieces per casting run.
How do you ensure zero-leakage performance under bi-directional flow conditions?
Our concentric butterfly designs utilize an engineered interference fit between the spherically machined disc edge and the precision-molded elastomeric seat arch. The disc edge is super-finished to an Ra < 0.4 μm mirror surface, minimizing frictional abrasion. Under reverse pressure, the line pressure forces the flexible elastomer against the rigid body bore, reinforcing contact pressure at the sealing line and guaranteeing ISO 5208 Rate A (zero detectable bubbles) in both flow directions.
Can our valves be certified for regional potable water and fire protection schemes?
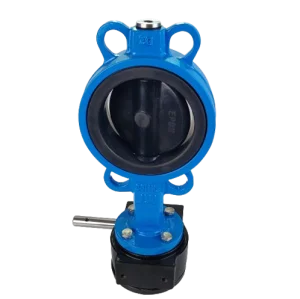
Yes. Our virgin EPDM formulations are batch-certified for international drinking water directives, including WRAS (UK), NSF/ANSI 61 (North America), ACS (France), and DVGW (Germany). For fire protection lines, our lug-type and grooved-end ductile iron butterfly units comply with UL/FM standards, featuring factory-fitted internal supervisory tamper switches and Class 150/PN16 pressure ratings.
Connect with our Engineering Foundry Team
Send your valve schedules, CAD drawings, or process specifications directly to our engineering specialists. Receive detailed project calculations, general arrangement drawings, and quotation packs within 24 hours.
